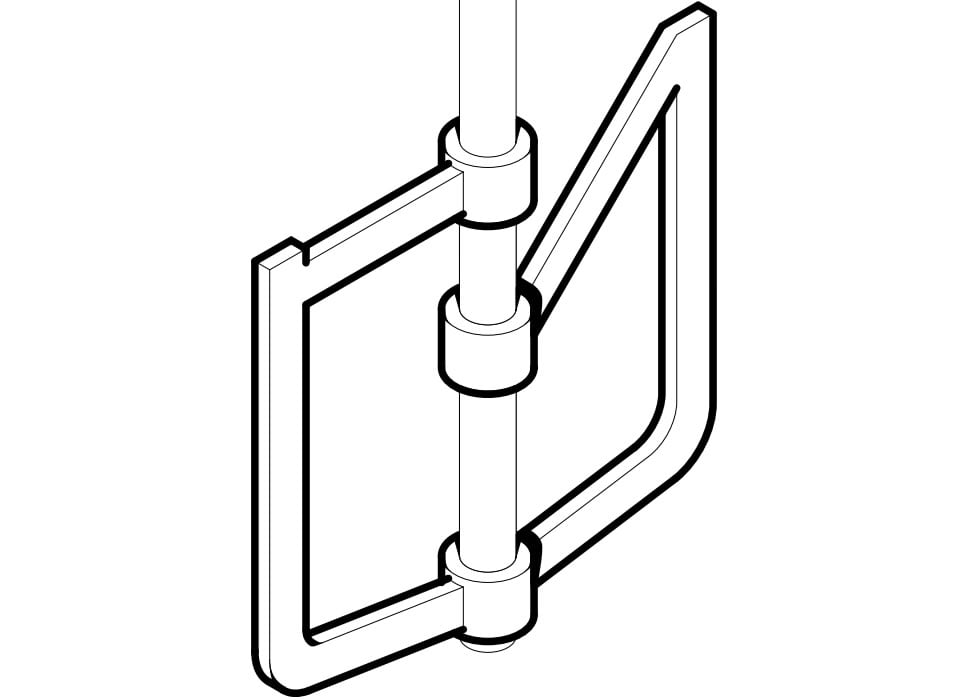
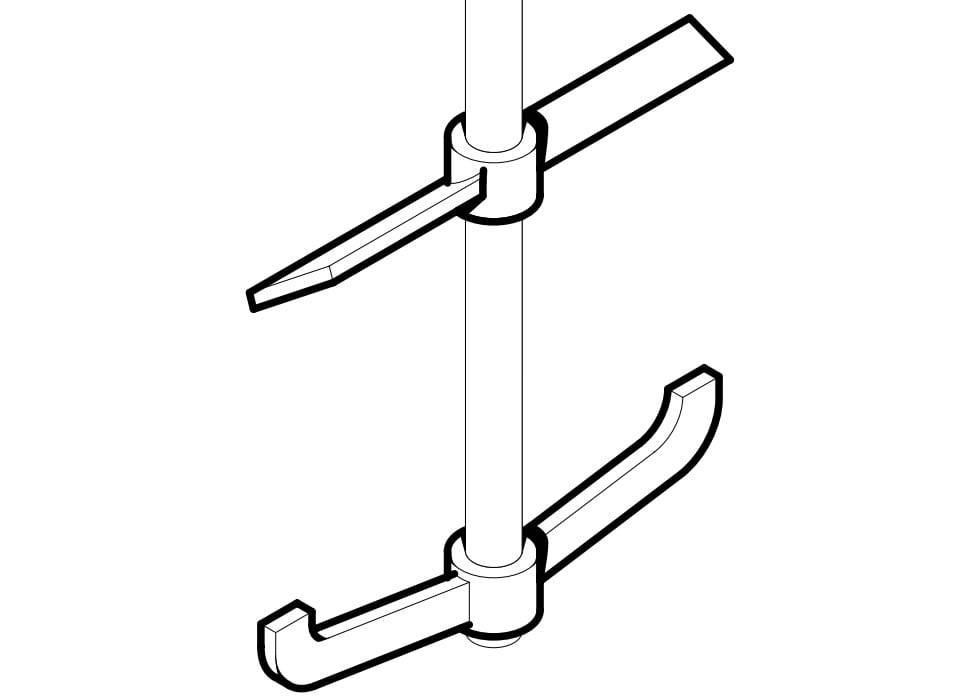
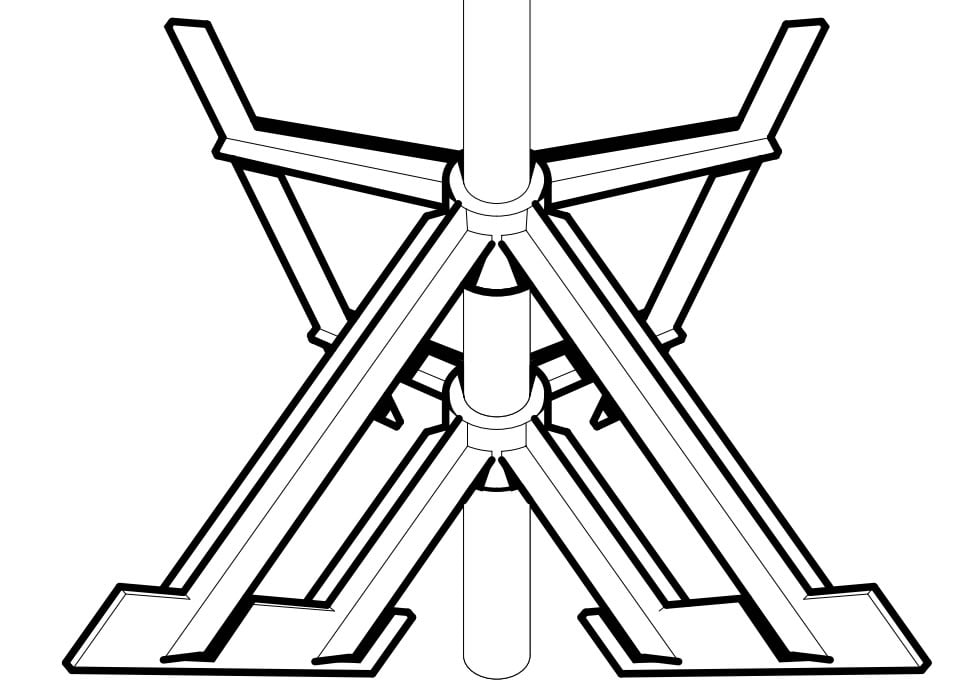
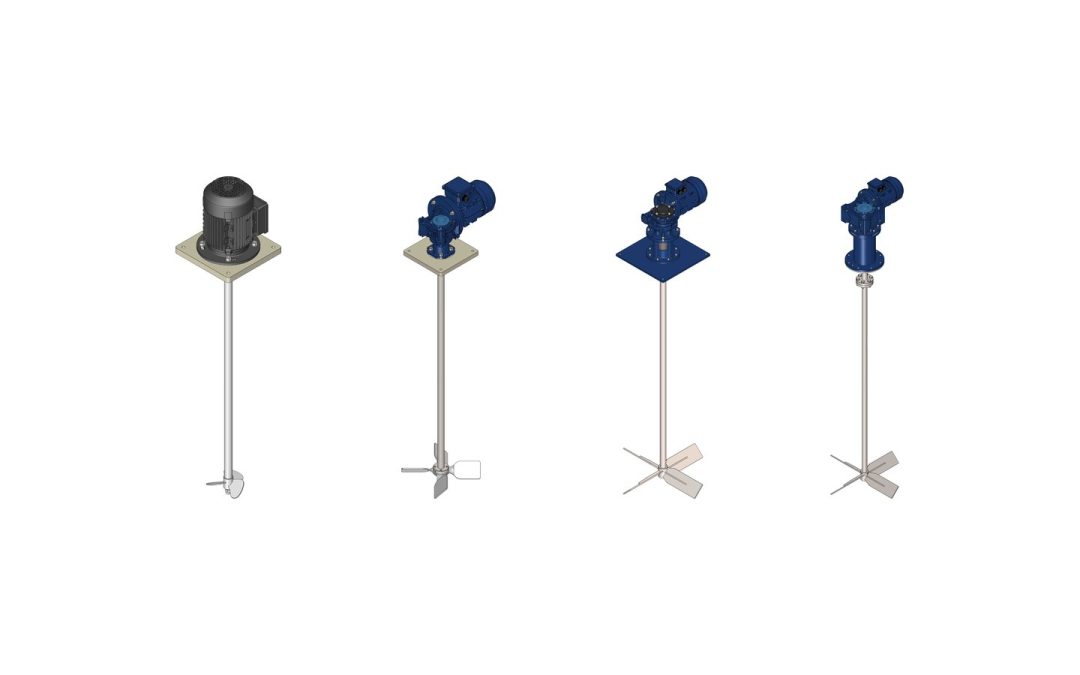
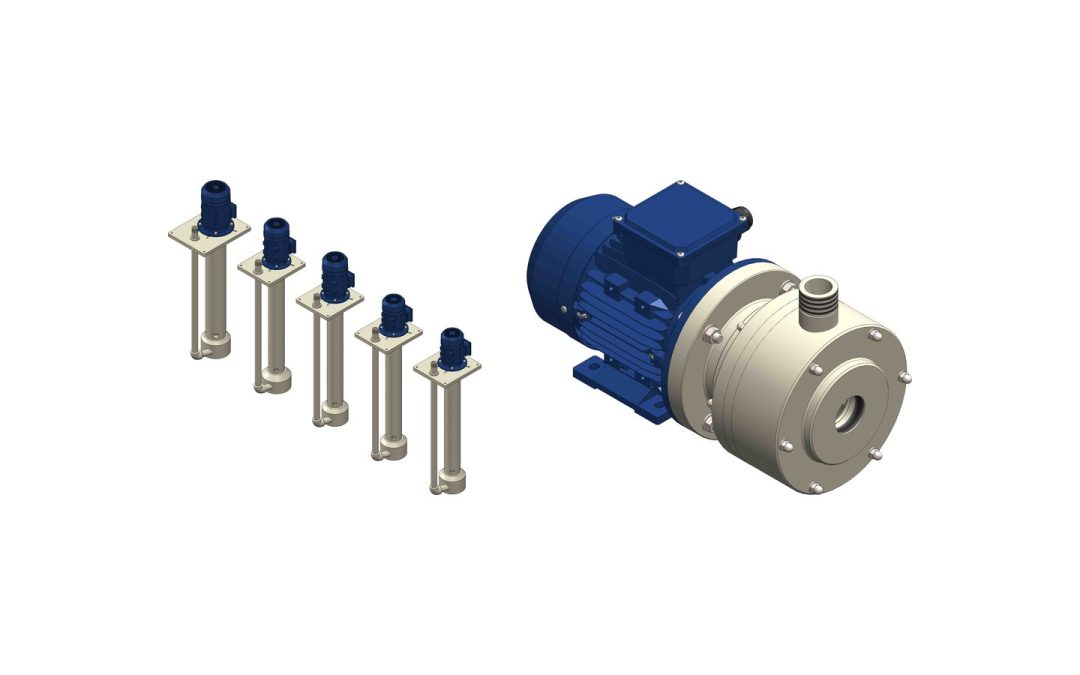
Put two agitators with the same motor and shaft into the same tank and you can still get opposite results. The difference is the impeller. Different agitator impeller types decide how the fluid moves, how much shear reaches droplets, bubbles and agglomerates, and how much motor power becomes useful mixing rather than heat and vortex.
This guide reviews the impellers we fit at Nuova Darimpianti on agitators for corrosive service: marine propeller, Cowles (cowless) disc, Rushton turbine, emulsifier, folding blades, pitched blades, high-flow, anchor and scraper. For each one we cover flow, viscosity, uses and limits. For the full agitator selection process (process objective, Reynolds number, motor), start with how to choose an industrial agitator; here we stay on the impeller.
Axial, radial and tangential flow
Every impeller pushes fluid in a dominant direction, and that direction sets the job it does well.
Axial flow
Axial impellers push liquid parallel to the shaft, usually towards the bottom. The jet rises along the walls and returns to the impeller, forming a single loop that sweeps the whole volume. This is the most efficient pattern for blending, keeping solids suspended and evening out temperature with little power. Marine propellers, pitched blades (mixed flow with an axial bias) and high-flow impellers belong here.
Radial flow
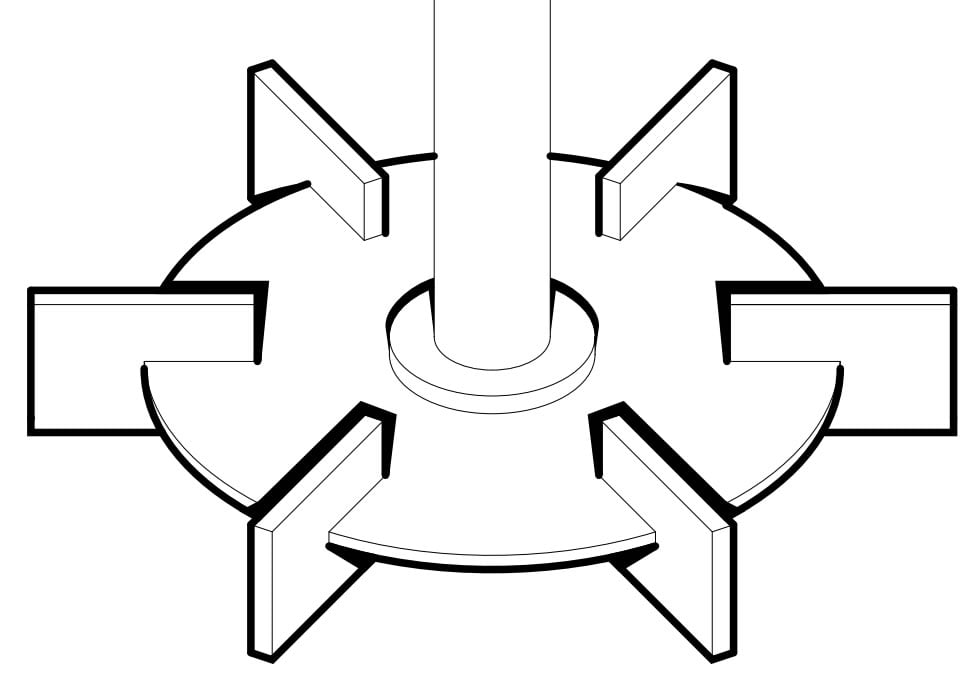
Radial impellers discharge fluid towards the walls, creating two loops above and below the impeller. They pump less liquid per kW but concentrate a lot of shear close to the blades: what you need to disperse powders and pigments, break agglomerates, emulsify or break up a gas. Cowles discs, Rushton turbines and emulsifiers are radial.
Tangential flow
Anchors and scrapers turn slowly with a diameter close to the tank diameter, dragging the fluid round and acting continuously on the wall. You need them when the product is so viscous that a small impeller would only stir a “cavern” of liquid around itself.
In unbaffled cylindrical tanks, fast impellers tend to spin the whole liquid and pull a central vortex. The usual fixes are baffles, off-centre or angled mounting and side-entry agitators. Anchors, by contrast, run without baffles.
Agitator impeller types one by one
Speeds quoted are those on our product datasheets. Viscosity ranges are indicative and should be checked against the real fluid.
Three-blade marine propeller
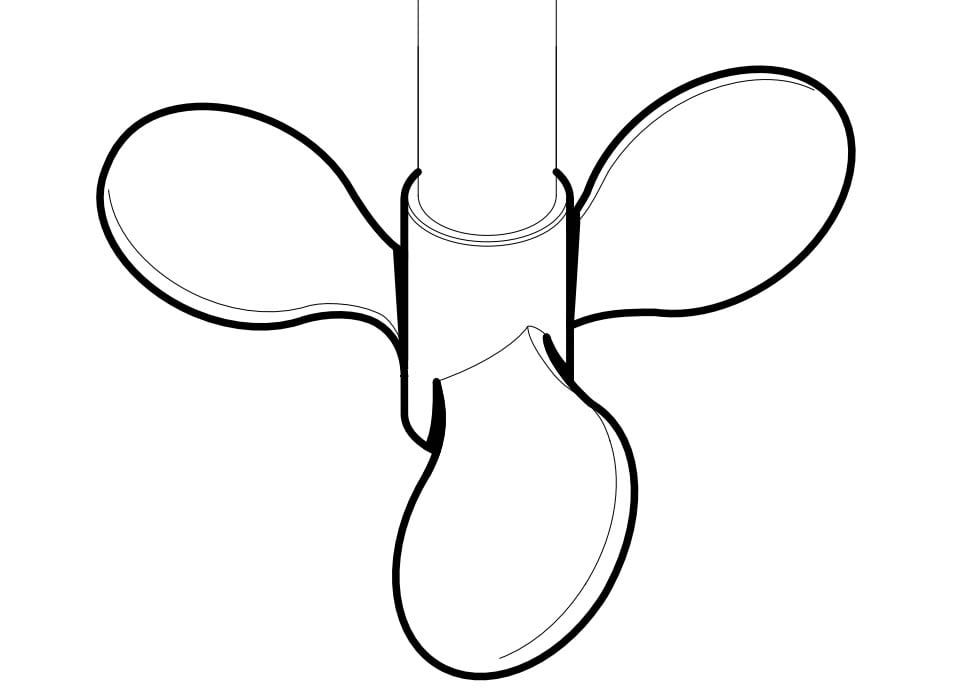
The most common impeller on fast agitators: three helical blades driving liquid towards the bottom with clean axial flow and low power. It runs from 500 to 1,500 rpm and is the standard impeller on the EV and EVK ranges.
Viscosity: low, up to about 2,000-3,000 cP.
Typical uses: diluting and neutralising acids and alkalis, preparing solutions, water treatment.
Strengths: high flow per kW, low vibration.
Limits: little shear; in viscous fluids the flow dies out near the impeller.
Cowles (cowless) disc impeller
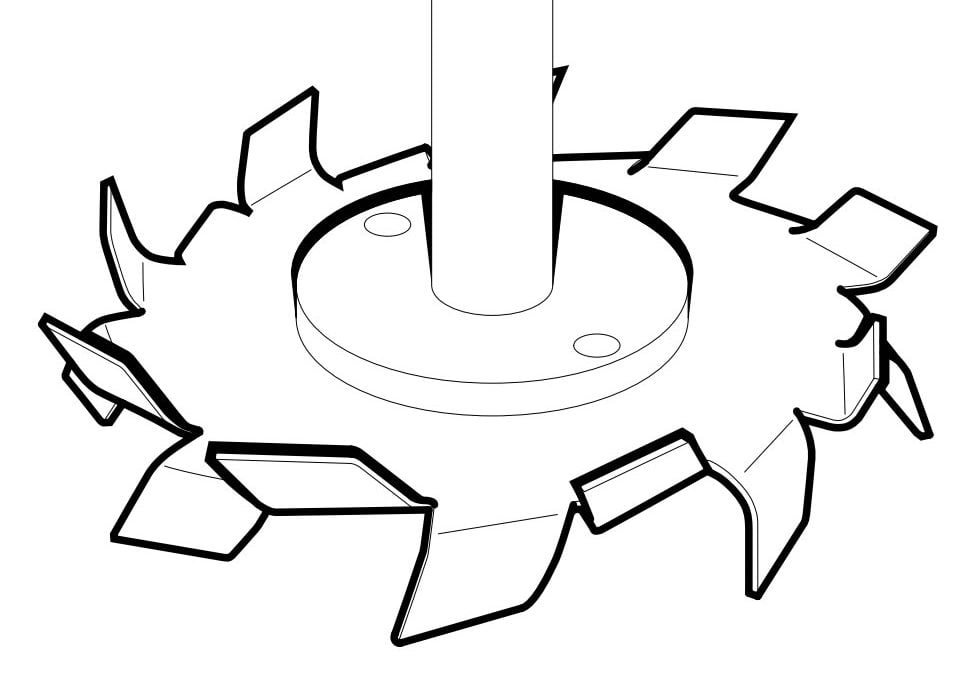
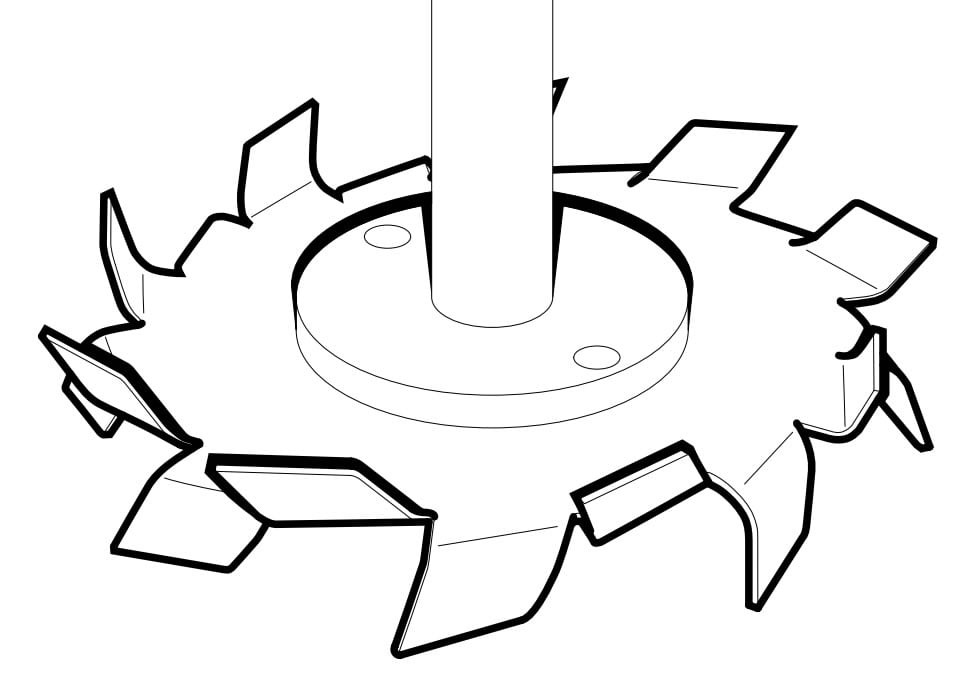
The Cowles impeller, often spelled “cowless” and also called a toothed disc or disperser blade, is a disc with teeth bent alternately up and down. At high speed it creates a very intense shear zone at the rim while product is drawn in from above and below and thrown towards the walls. It has the widest range in our line-up: 300 to 3,000 rpm. In dispersers the disc tip speed matters more than rpm (see sizing below).
Viscosity: from thin liquids to pastes of a few tens of thousands of cP, as long as product keeps flowing back to the disc.
Typical uses: dispersing pigments and fillers in paints and inks, fast powder dissolution, breaking agglomerates.
Strengths: very high shear from a simple, easy-to-clean geometry.
Limits: low pumping, so large tanks need a second circulation impeller; high power draw at top speed.
Straight-blade Rushton turbine
Six flat vertical blades on a disc. The disc stops gas sparged from below escaping up the shaft and forces it through the blades, where it is broken up. It runs from 300 to 1,400 rpm.
Viscosity: low to medium, below about 5,000 cP.
Typical uses: gas-liquid dispersion, reactions needing high mass transfer.
Strengths: high local turbulence, well-documented behaviour.
Limits: high power number; needs baffles; inefficient for plain blending.
Emulsifier impeller
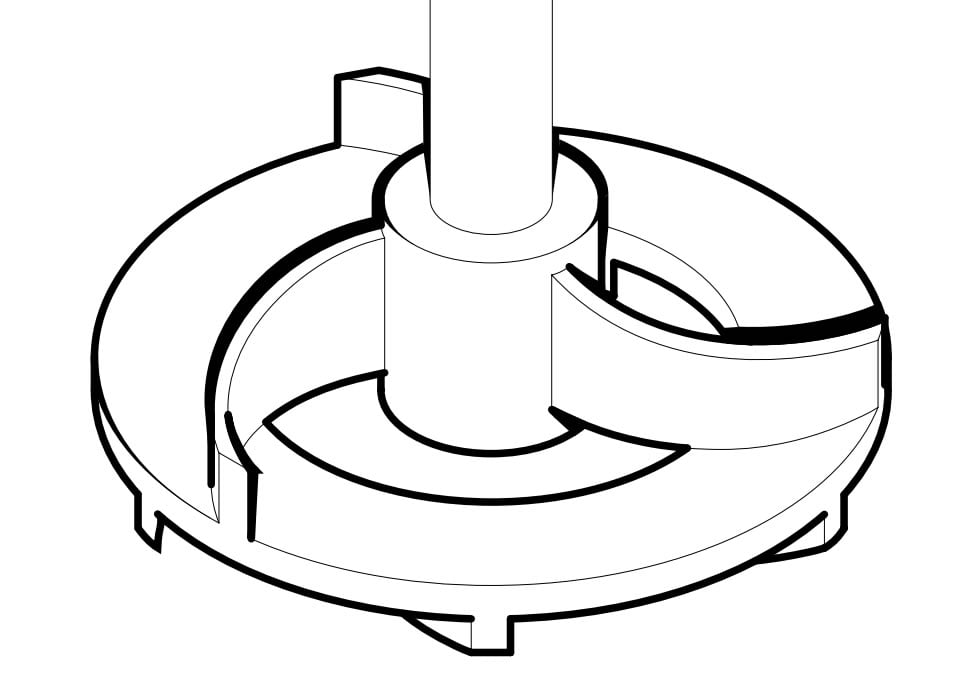
Curved vanes inside a toothed ring: liquid enters at the centre, is accelerated and leaves through the ring, where it is sheared hard and repeatedly. It runs from 500 to 2,000 rpm.
Viscosity: low to medium.
Typical uses: emulsions of immiscible phases, fine and stable dispersions.
Strengths: smaller, more uniform droplets than an open impeller.
Limits: modest circulation; more sensitive to coarse solids.
Folding-blade (movable-blade) impellers
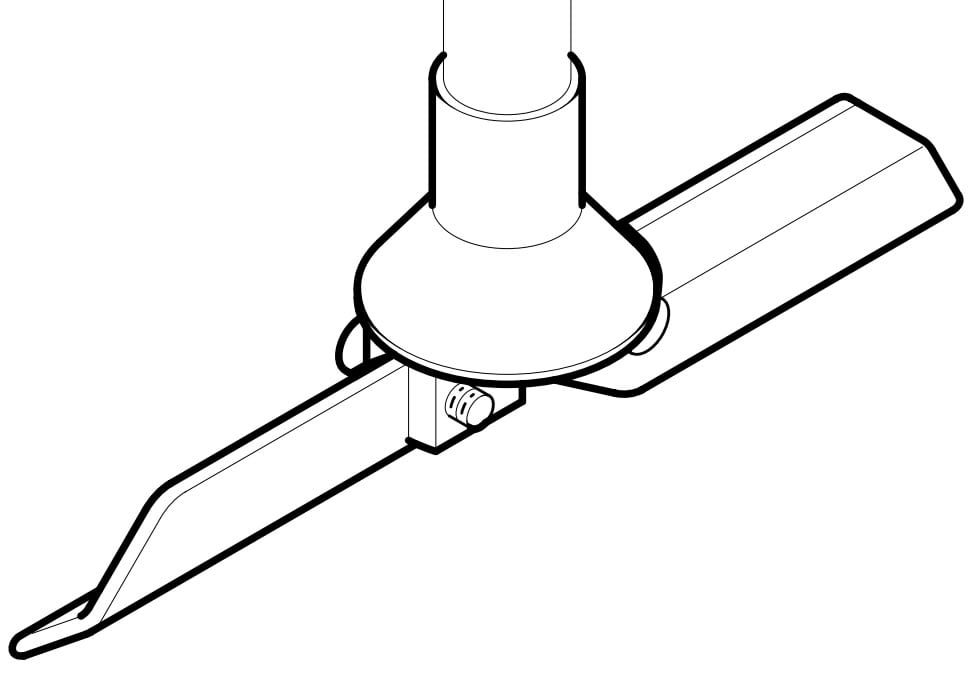
Folding-blade agitators are built for containers with a small opening, such as IBC totes and drums. The blades are pinned to the hub: in the usual arrangement they hang along the shaft when stopped, pass through the filler neck, then swing open as the shaft turns and work at full diameter. Our datasheets list the movable-blade impeller in the fast range (300-1,500 rpm) and, as a four-blade version, in the slow range (up to 400 rpm).
Viscosity: low to medium.
Typical uses: re-mixing additives and reagents in IBCs, re-suspending settled solids.
Strengths: working diameter larger than the opening; one agitator can serve several totes.
Limits: the hinge needs checking with solids-laden or crystallising fluids.
Pitched-blade turbine and modular impeller
Four flat blades set at an angle, usually 45°, give mixed flow with an axial bias. It is the workhorse of slow agitators: the pitched-blade turbine and modular pitched-blade impeller run from 10 to 380 rpm. The four-blade impeller also comes with straight blades when more radial action is needed.
Strengths: versatile; several impellers can be stacked in tall tanks.
Limits: draws more power than a high-flow impeller for the same flow.
High-flow four-blade impeller
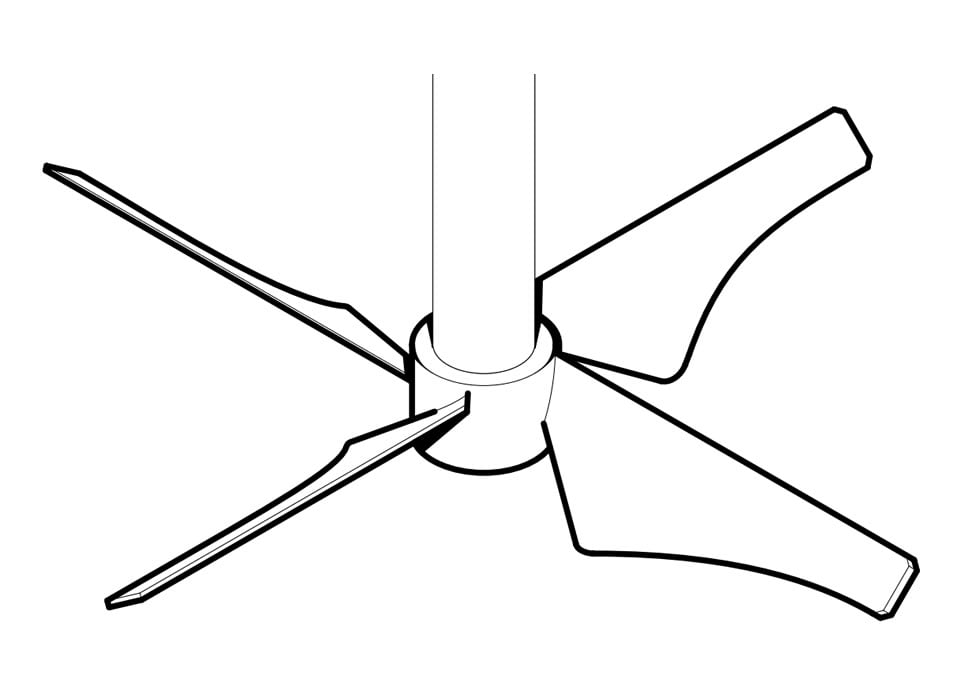
Profiled blades, wide at the root and tapering to the tip, designed to move the most volume with the least shear. It runs from 10 to 380 rpm on the EVRK, EVRL and KVRL ranges and the LRO side-entry mixer.
Viscosity: low, best below about 1,000 cP.
Typical uses: large tanks, solids suspension, flocculation where flocs must not break.
Strengths: low power number, so smaller gear motors.
Limits: loses effectiveness as viscosity rises; unsuited to dispersion.
Anchor impeller: gate anchor and anchor with paddle
The anchor follows the tank profile close to wall and bottom, turns slowly (5-56 rpm on our datasheets) and moves the whole batch by drag. The version with a paddle adds an upper arm that improves vertical turnover, the weak point of a plain anchor.
Strengths: moves the whole volume; improves heat transfer at the wall.
Limits: poor vertical exchange without extra paddles; high torque.
Scraper impeller
The scraper takes the anchor idea to its limit: arms and shoes work almost in contact with bottom and walls, removing product that sticks, settles or crystallises. We design scrapers to order around the tank and the product.
Viscosity: high, or products that build deposits.
Typical uses: fouling products, sludges that compact, wall-heated tanks.
Strengths: clean walls and bottom, steady heat transfer.
Limits: shoe wear; high power and starting torque.
Impeller comparison table
Impeller
Flow
Indicative viscosity
Speed (Nuova Darimpianti datasheets)
Typical applications
Three-blade marine propeller
Axial
Up to 2,000-3,000 cP
500-1,500 rpm
Dilution, neutralisation, water treatment
Cowles (cowless) disc
Radial, very high shear
Thin liquids to pastes
300-3,000 rpm
Pigment dispersion, powder dissolution
Rushton turbine
Radial
Below 5,000 cP
300-1,400 rpm
Gas dispersion, reactions
Emulsifier
Radial, high shear
Low-medium
500-2,000 rpm
Emulsions, fine dispersions
Folding blades
Mixed
Low-medium
300-1,500 rpm (fast); up to 400 rpm (slow)
IBCs, drums, narrow openings
Pitched blade / modular
Mixed, mainly axial
Up to about 10,000 cP
10-380 rpm
Flocculation, polyelectrolyte, plating
High-flow four-blade
Axial
Below about 1,000 cP
10-380 rpm
Large tanks, solids suspension
Anchor (gate / with paddle)
Tangential
5,000 to over 50,000 cP
5-56 rpm
Resins, gels, jacketed tanks
Scraper
Tangential with wall scraping
High or fouling
Custom design
Products that foul or settle
Sizing basics: D/T ratio, tip speed and power number
The D/T ratio
D is the impeller diameter, T the tank diameter. Typical values: 0.2-0.35 for marine propellers, 0.25-0.4 for Cowles discs and Rushton turbines, 0.3-0.5 for pitched-blade and high-flow impellers, 0.9-0.98 for anchors and scrapers. Too small a D/T leaves dead zones; too large, on a fast impeller, sends power soaring.
Tip speed
The velocity of the blade tip:
v = π · D · N / 60
with v in m/s, D in metres and N in rpm. A 150 mm Cowles disc at 3,000 rpm reaches about 23.6 m/s, typical for dispersers; a 1.5 m anchor at 20 rpm about 1.6 m/s. Tip speed is the most direct indicator of shear and the figure to watch on thermoplastic impellers, which tolerate lower tip speeds than steel.
Power number and power draw
In turbulent flow, in a baffled tank:
P = Np · ρ · N³ · D⁵
with P in watts, ρ in kg/m³, N in revolutions per second and D in metres. Np depends on geometry: about 0.3-0.5 for marine propellers and high-flow impellers, 1.2-1.5 for a 45° four-blade turbine, about 5 for a Rushton.
Example: a 0.2 m propeller at 900 rpm (15 rev/s) in water, Np = 0.35: P = 0.35 × 1,000 × 15³ × 0.2⁵ ≈ 380 W. A Rushton of the same size at the same speed takes over 5 kW. Doubling speed multiplies power by 8, doubling diameter by 32, and power scales with density: in concentrated sulphuric acid (about 1,840 kg/m³) the same agitator draws nearly twice as much as in water. The motor is then chosen with a margin over this figure. In laminar flow the formula no longer applies in this form: anchors and scrapers are sized on torque. The link between viscosity and flow regime is covered in fast vs slow agitators.
Impeller materials for corrosive service
Choose the material for the worst product the impeller will see, at the highest temperature. On our fast ranges impellers come in AISI 304-316 stainless steel or in PP, PVC or PVDF; on the slow ranges also in PE-HD, and on the KVRL they can be ebonite-coated.
PP: dilute acids and alkalis, plating baths, water treatment, up to 80-90°C.
PVC: stiff and economical, but limited to 60°C.
PVDF: concentrated acids, strong oxidisers, up to 100-120°C.
AISI 304-316: with compatible fluids, for the highest tip speeds.
Matching impellers to fast, slow and side-entry agitators
Fast agitators. On EV/EV-G and EVK the standard impeller is the three-blade marine propeller. The EVL range, with a single or double bearing lantern, and the KVL also take the straight-blade turbine, emulsifier and Cowles disc: these are the machines to choose when the impeller draws more power or runs at high tip speed.
Slow agitators. The EVR range, with the shaft keyed directly to the gearbox, carries the four-blade impeller with pitched or straight blades; EVRK and EVRL add the high-flow impeller and a lantern for medium and high loads. The KVRL, built for heavy loads, can carry 2 to 4 two-blade or four-blade impellers on one shaft, the answer for tall tanks or variable levels.
Side-entry agitators. The fast LVO takes the propeller, straight-blade turbine, emulsifier or Cowles disc; the slow LRO takes the four-blade impeller with pitched, straight or high-flow blades. Side entry suits large tanks and helps avoid a central vortex.
Frequently asked questions
What is the difference between a Cowles (cowless) impeller and a Rushton turbine?
Both produce radial flow. The Cowles disc concentrates very intense shear at the rim and is designed to disperse powders and pigments at high tip speed. The Rushton has flat blades on a disc, spreads turbulence more evenly and is the classic choice for dispersing gas into a liquid.
What are folding-blade agitators?
Agitators whose blades are hinged at the hub, so they fold to pass through a narrow opening and open as the shaft turns. They are mainly used to mix IBC totes and drums, where a rigid impeller of the required diameter would not fit through the filler neck.
Which impeller should I use for a very viscous fluid?
Above roughly 5,000-10,000 cP, small fast impellers only move the liquid around them. Use an anchor, possibly with an upper paddle, or a scraper if the product sticks to the walls. They run slowly, our anchor from 5 to 56 rpm, with gearboxes sized on torque.
Can I fit more than one impeller on the same shaft?
Yes, it is standard in tall tanks. The KVRL range takes 2 to 4 two-blade or four-blade impellers. Dispersion processes often pair a shear impeller, such as a Cowles disc, with an axial circulation impeller, to be assessed case by case.
Plastic or steel impeller?
It depends on the fluid and the tip speed. With acids, alkalis and oxidisers, PP, PVC and PVDF avoid corrosion; with compatible fluids and very high tip speeds, AISI 304-316 steel gives more mechanical margin. Often the answer is a coated steel shaft with a thermoplastic impeller machined from solid.
Conclusion: start from the flow you need
Choosing between agitator impeller types starts with one question: what has to happen in the tank? For circulation, look at axial impellers (marine propeller, pitched blade, high-flow); for shear, at radial ones (Cowles disc, Rushton, emulsifier); for thick products or fouling walls, at anchors and scrapers. Then check D/T, tip speed and power, and choose the material for the most aggressive fluid.
Choosing an impeller for a new agitator, or replacing one that underperforms? Nuova Darimpianti’s engineering team in Flero (Brescia, Italy) has been designing and building agitators and impellers in PP, PVC, PVDF and stainless steel for corrosive fluids since 1970, including custom designs. Send us your fluid, viscosity, volume and tank geometry: contact us for a no-obligation technical consultation.
Anyone who designs or runs a plant handling corrosive fluids eventually faces a very practical question: will this material withstand this chemical, at this concentration, at this temperature? This chemical resistance chart for polymers brings together the substances that come up most often in our customers’ enquiries: more than 40 combinations of acids, alkalis, oxidisers, salts and solvents, rated for polypropylene (PP), PVC and PVDF at 20 °C and 60 °C, with a room-temperature comparison against PE-HD, PTFE and AISI 316 stainless steel.
Important notice. The ratings below are indicative. They are based on general technical literature and on the compatibility charts published by manufacturers of semi-finished plastics. They refer to single substances in aqueous solution, at atmospheric pressure and without significant mechanical stress. They do not replace a check on your specific application: before choosing the material for a pump, an agitator or a tank, always confirm the data with the material supplier and the equipment manufacturer.
How to read the chemical resistance chart for polymers
Each cell combines three pieces of information: the chemical, its concentration and the temperature of the fluid in contact with the material. The rating scale is deliberately simple:
A, resistant: suitable for continuous service. Slight changes in colour or weight may occur without affecting function.
B, limited resistance: moderate attack (swelling, loss of mechanical properties, surface oxidation). It may be acceptable for short contact, unstressed parts or a shorter service life, but needs a case-by-case assessment.
C, not recommended: rapid or severe attack. Do not use.
–, insufficient data: no reliable general data, or published sources disagree. Testing is required.
Concentrations are given in percent by weight, except sodium hypochlorite, which is expressed as available chlorine as on commercial data sheets. The PVC 60 °C column sits at the material’s operating limit: even where chemical resistance is good, the mechanical margin at that temperature is small. For PE-HD, PTFE and AISI 316 we only show the 20 °C value, because they are included as reference materials rather than as the main construction materials of our pumps.
Where the sources we consulted disagreed, we chose the more cautious rating. In a chart like this, erring on the side of caution costs you a more expensive material at worst; erring on the side of optimism can cost you a plant shutdown or a product leak.
Maximum operating temperatures
Temperature matters before chemical compatibility does. A material that is chemically suitable but used beyond its thermal limit deforms, loses stiffness and becomes more vulnerable to attack by the fluid. The figures below match those in our thermoplastics guide and refer to pump and agitator components in continuous service.
Material
Max operating temperature (indicative)
Notes
PP (polypropylene)
80–90 °C
Depends on grade and mechanical load; brittle below 0 °C
PVC (polyvinyl chloride)
60 °C
Loses dimensional stability above 60 °C
PVDF (polyvinylidene fluoride)
100–120 °C
Good dimensional stability under load at temperature
PE-HD (high-density polyethylene)
60–70 °C
Less rigid than PP; good toughness at low temperature
PTFE
up to ~250 °C
Literature value; mainly used for gaskets and linings
AISI 316
not the limiting factor
Corrosion (chlorides, reducing acids) sets the limit, not temperature
For pumps, the real limit also depends on the design: our PMC-1 horizontal pumps with mechanical seal are rated for temperatures up to 80 °C, while the HTM magnetic drive pump, in PP or PVDF, and the VGA vertical pump go up to 90 °C.
Chemical resistance chart: inorganic acids
Mineral acids are where thermoplastics clearly outperform metals. Hydrochloric acid attacks stainless steel even when dilute, while PP, PVC and PVDF handle it well. Oxidising acids are a different story: concentrated nitric acid and chromic acid oxidise the hydrocarbon chains of PP and PE, and PVDF becomes the safer choice.
Chemical
Conc.
PP 20 °C
PP 60 °C
PVC 20 °C
PVC 60 °C
PVDF 20 °C
PVDF 60 °C
PE-HD 20 °C
PTFE 20 °C
AISI 316 20 °C
Sulphuric acid
≤ 10%
A
A
A
A
A
A
A
A
B
Sulphuric acid
50%
A
A
A
B
A
A
A
A
C
Sulphuric acid
96–98%
B
C
B
C
A
A
B
A
B
Oleum (fuming sulphuric acid)
–
C
C
C
C
C
C
C
A
–
Hydrochloric acid
≤ 10%
A
A
A
A
A
A
A
A
C
Hydrochloric acid
37%
A
B
A
B
A
A
A
A
C
Nitric acid
≤ 10%
A
B
A
B
A
A
A
A
A
Nitric acid
40%
B
C
B
C
A
B
B
A
A
Nitric acid
65%
C
C
C
C
A
B
C
A
A
Phosphoric acid
85%
A
A
A
B
A
A
A
A
B
Hydrofluoric acid
40%
A
C
C
C
A
A
A
A
C
Chromic acid
≤ 20%
B
C
B
C
A
A
B
A
B
A few notes on these ratings:
Concentrated sulphuric acid. At 96–98% PP tends to oxidise and darken even at room temperature; PVDF handles it at elevated temperature too. Oleum, which contains free SO3, attacks every thermoplastic in the chart.
Hydrochloric acid 37%. PP and PVC are resistant, but concentrated HCl slowly permeates through the walls. Staining on the outer surfaces of tanks and pipes, and corrosion of nearby metal parts, are common side effects.
Hydrofluoric acid. PE-HD is often preferred to PP for dilute solutions because it is less prone to stress cracking. PVC is not recommended. For high concentrations or temperatures above 40 °C, use PVDF.
Chromic acid. PP and PVC are used in chrome plating baths at moderate temperature, but service life depends heavily on concentration and temperature. That variability is why we rate them B at 20 °C and C at 60 °C.
Organic acids
Organic acids are generally less aggressive than mineral acids, with one important exception: glacial acetic acid swells PVC and should be handled in PP or PVDF.
Chemical
Conc.
PP 20 °C
PP 60 °C
PVC 20 °C
PVC 60 °C
PVDF 20 °C
PVDF 60 °C
PE-HD 20 °C
PTFE 20 °C
AISI 316 20 °C
Acetic acid
10%
A
A
A
A
A
A
A
A
A
Glacial acetic acid
≥ 96%
A
B
C
C
A
B
B
A
A
Formic acid
85%
A
B
B
C
A
B
A
A
B
Citric acid
aqueous sol.
A
A
A
A
A
A
A
A
A
Oxalic acid
aqueous sol.
A
A
A
A
A
A
A
A
B
Alkalis and caustic solutions
With strong alkalis the ranking between materials reverses. PP and PE-HD resist caustic soda and caustic potash at all common concentrations, including at elevated temperature. PVDF, despite being the most resistant material with acids, can discolour and crack in contact with hot concentrated alkalis. In concentrated caustic soda circuits above 50 °C, PP is more reliable than PVDF.
Chemical
Conc.
PP 20 °C
PP 60 °C
PVC 20 °C
PVC 60 °C
PVDF 20 °C
PVDF 60 °C
PE-HD 20 °C
PTFE 20 °C
AISI 316 20 °C
Sodium hydroxide (caustic soda)
10%
A
A
A
A
A
B
A
A
A
Sodium hydroxide (caustic soda)
50%
A
A
A
B
B
C
A
A
A
Potassium hydroxide
50%
A
A
A
B
B
C
A
A
A
Ammonia (aqueous solution)
25%
A
A
B
C
A
B
A
A
A
Calcium hydroxide (milk of lime)
slurry
A
A
A
A
A
A
A
A
A
Concentrated ammonia attacks PVC; aliphatic amines (not listed) also attack PVDF and should always be checked.
Salts, oxidisers and process solutions
Salt solutions are rarely a problem for thermoplastics. They are a problem for AISI 316: chlorides and ferric chloride cause pitting corrosion, even at room temperature. With oxidisers such as hypochlorite, hydrogen peroxide and chlorine, temperature and concentration decide everything.
Chemical
Conc.
PP 20 °C
PP 60 °C
PVC 20 °C
PVC 60 °C
PVDF 20 °C
PVDF 60 °C
PE-HD 20 °C
PTFE 20 °C
AISI 316 20 °C
Sodium hypochlorite
≤ 5% av. Cl
A
B
A
B
A
A
A
A
C
Sodium hypochlorite
12–15% av. Cl
B
C
A
B
A
B
B
A
C
Hydrogen peroxide
≤ 30%
B
C
B
C
A
B
A
A
A
Hydrogen peroxide
50%
C
C
C
C
A
B
B
A
A
Chlorine (wet gas)
–
C
C
B
C
A
A
C
A
C
Ferric chloride
saturated sol.
A
A
A
A
A
A
A
A
C
Sodium chloride (brine)
saturated sol.
A
A
A
A
A
A
A
A
B
Copper / nickel sulphate
saturated sol.
A
A
A
A
A
A
A
A
A
Demineralised water
–
A
A
A
A
A
A
A
A
A
Sodium hypochlorite. PVC is the traditional material for storage and dosing. PP works well with cold, dilute solutions, but with commercial product at 12–15% available chlorine it oxidises progressively, especially when also exposed to light.
Hydrogen peroxide. Cleanliness and the absence of metal contaminants, which catalyse decomposition, matter as much as the material. Above 30%, PVDF is the only thermoplastic in the chart with an adequate margin.
Solvents and hydrocarbons
No general rule applies to organic solvents: each chemical family has to be considered on its own. PVDF resists aromatic and chlorinated hydrocarbons very well, where PP, PE and PVC swell or dissolve, but it is attacked by ketones (acetone, MEK) and dissolves in polar aprotic solvents such as DMF and NMP, which PP tolerates.
Chemical
Conc.
PP 20 °C
PP 60 °C
PVC 20 °C
PVC 60 °C
PVDF 20 °C
PVDF 60 °C
PE-HD 20 °C
PTFE 20 °C
AISI 316 20 °C
Methanol
100%
A
A
A
B
A
A
A
A
A
Ethanol
96%
A
A
A
B
A
A
A
A
A
Isopropanol
100%
A
A
A
B
A
A
A
A
A
Acetone
100%
B
C
C
C
C
C
B
A
A
Methyl ethyl ketone (MEK)
100%
B
C
C
C
C
C
B
A
A
Ethyl acetate
100%
B
C
C
C
B
C
B
A
A
Toluene / xylene
100%
C
C
C
C
A
B
C
A
A
Dichloromethane
100%
C
C
C
C
B
C
C
A
A
Trichloroethylene / perchloroethylene
100%
C
C
C
C
A
B
C
A
A
Dimethylformamide (DMF)
100%
A
B
C
C
C
C
A
A
A
Diesel / mineral oils
–
B
C
A
B
A
A
B
A
A
Manufacturers’ charts are not consistent on ketones and esters: some rate PP as resistant to acetone at 20 °C, others as limited. We chose B. Rigid PVC is unsuitable for every solvent in the chart except the alcohols.
Factors that change chemical resistance
A chart summarises how a material behaves under standard conditions. In a real plant other factors come into play, and they can turn an A into a B, or a B into a C.
Concentration
Resistance does not always change linearly with concentration. Dilute sulphuric acid is mild for PP; at 98% it is an oxidiser. Check the actual concentration in service, including changes caused by evaporation or topping up.
Temperature
As a rule of thumb, every 10 °C rise noticeably speeds up chemical reactions and the diffusion of the fluid into the polymer. A material rated A at 20 °C can drop to B or C at 60 °C. Design for the maximum temperature reached, not the average: peaks during cleaning, exothermic dilution (sulphuric acid is the classic case) and heating cycles matter more than the nominal value.
Mixtures
The chart rates one chemical at a time. Mixtures can behave very differently: nitric acid combined with hydrofluoric acid, sulphuric acid with oxidisers, or an acid solution containing traces of solvent can attack a material that resists each component on its own. Mixtures need a dedicated assessment and, for critical processes, an immersion test.
Mechanical stress and stress cracking
A loaded component (a rotating impeller, a shaft, a bolted flange) is more vulnerable than an unstressed test specimen. Environmental Stress Cracking, the cracking caused by stress and fluid acting together, mainly affects polyolefins in contact with surfactants, alcohols and some oxidisers. Residual stresses in moulded parts make the problem worse; this is why the critical components of our pumps are machined from solid, as explained in our article on solid block CNC machining.
Permeation
Some small molecules, such as HCl, chlorine, bromine and certain solvents, slowly pass through polymer walls without visibly degrading them. Permeation does not necessarily damage the plastic part, but it can corrode external metal parts (bolts, frames, motors) or contaminate the fluid. Thicker walls and fluoropolymers reduce it.
Seals and elastomers
The chart covers structural materials. In a pump the weakest link is often the O-ring or the seal: a PVDF casing with an incompatible gasket will still leak. Elastomers (FKM, EPDM) and PTFE must be selected with the same care, using their own compatibility charts.
From the chart to pump and agitator selection
The chart is a first screening tool. In practice the final choice also weighs cost, availability of semi-finished stock, mechanical loads and expected service life. Some practical pointers:
For dilute acids and alkalis at moderate temperature, PP covers most applications. It is the base material of our horizontal and vertical pumps.
For hypochlorite and cold applications where stiffness is needed, PVC remains a sound choice.
For concentrated acids, strong oxidisers, hydrofluoric acid and temperatures up to 100–120 °C, move to PVDF.
For agitators, the shaft can be AISI 304-316 stainless steel or steel coated with PP, PVC, PVDF or PE-HD. With chloride-rich fluids or reducing acids, the thermoplastic coating protects the steel, as on our EVL fast mixers.
For heating and cooling aggressive fluids we build heat exchangers in PP, PE, PVDF and PVC, as part of our special equipment range.
If your fluid is an acid, you will find guidance on pump configuration (single seal, double seal or magnetic drive) in our guide to pumps for corrosive acids. For surface treatment baths, where acids, metal salts and high temperatures coexist, see also our article on agitators for electroplating.
Frequently asked questions
What is the difference between “limited resistance” and “not recommended”?
With limited resistance (B) the material suffers moderate attack: it may swell, lose some mechanical properties or discolour. It can be acceptable for occasional contact or lightly stressed parts, but service life is shorter and must be assessed case by case. Not recommended (C) means rapid or severe attack: do not use the material under those conditions.
Is PVDF always the safest choice?
No. PVDF is the most resistant material with strong acids, oxidisers, aromatic and chlorinated hydrocarbons, but it resists hot concentrated alkalis less well than PP and is attacked by ketones, amines and solvents such as DMF and NMP. It also costs several times more than PP. Specify it when it is genuinely needed.
Can I use the chart for a mixture of chemicals?
Only as a first indication. Mixtures can be more aggressive than their individual components, for example nitric acid with hydrofluoric acid, or acids in the presence of oxidisers. A mixture needs a specific assessment and, in critical processes, an immersion test under real operating conditions.
Why does AISI 316 stainless steel rate worse than plastic with some acids?
AISI 316 relies on a passive oxide layer that holds up well in oxidising environments such as nitric acid, but is broken down by reducing acids (hydrochloric, dilute sulphuric) and by chlorides, which cause pitting. Under those conditions PP, PVC and PVDF last longer and cost less than special alloys.
How do I check compatibility for a specific application?
You need the fluid composition and concentration, minimum and maximum temperature, any suspended solids, the duty (continuous or intermittent) and the components involved. With that information the material suppliers’ charts can be cross-checked and, if the case is borderline, an immersion test carried out. Our technical department can run this check with you.
Check the material before you order
A chemical resistance chart narrows down the options quickly, but the final answer depends on the real application: fluid, concentration, temperature, mechanical loads and type of machine. In Flero (Brescia, Italy), Nuova Darimpianti designs and builds pumps and agitators in PP, PVC, PE-HD and PVDF machined from solid, with stainless steel or coated shafts, and has been helping customers choose the right material for decades.
Have a fluid to handle and not sure about the material? Contact our technical department with the chemical, concentration and temperature, and we will help you check compatibility and select the right pump or agitator.
Every plant that uses acids or alkalis has to move them somewhere. Sulphuric acid leaves a bulk tank and ends up in a neutralisation pit; caustic soda is drawn from storage and metered into a pH control loop; ferric chloride is pumped from an IBC to a flocculation tank. Chemical dosing and transfer systems are the pumps, tanks, pipework, valves and instruments that do this work. Specified well, they run for years with little attention. Specified badly, they produce a steady stream of failed seals, cavitating pumps, corroded floors and operators exposed to acid fumes.
This guide is written for process engineers, plant managers and buyers who need to specify, upgrade or replace a system for withdrawing, transferring and dosing corrosive liquids. It covers the main components, how to match materials to the chemical, the design choices that keep leaks under control, and the data you need before asking for a quote. The last section explains how Nuova Darimpianti, based in Flero near Brescia, Italy, designs and builds these systems to order, from a single pump to a complete skid.
What chemical dosing and transfer systems do
Three functions are usually involved, often in the same installation:
Withdrawal: taking liquid out of a storage tank, pit or drum.
Transfer and recirculation: moving it to a day tank, a process vessel or a treatment line, or keeping it circulating through a filter, heat exchanger or scrubber.
Dosing: injecting a controlled quantity of chemical into a process, for example acid for pH correction, caustic for neutralisation, or coagulant and polyelectrolyte for water treatment.
A typical layout therefore includes a storage tank, a transfer pump, sometimes a make-up tank with an agitator where the chemical is diluted or dissolved, a dosing pump, the valves and instruments that protect each item, and secondary containment around the whole lot. Where the chemical gives off fumes, tank vents are routed to an abatement system.
The difference from an ordinary water circuit is the fluid. A concentrated acid attacks metals, swells the wrong elastomers and turns a small drip into a safety incident. Every wetted part has to be compatible with the chemical, and the layout should keep the number of potential leak points as low as possible.
The main components
Withdrawal from tanks: vertical immersion pumps
For drawing liquid from an open-top tank or pit, the usual answer is a vertical centrifugal pump. The pump casing sits submerged in the liquid while the motor stays above the rim, so the pump is always flooded, needs no priming and has practically no suction line. That removes the most common cause of cavitation (suction-side losses) along with a whole set of flanges and fittings that could leak.
Nuova Darimpianti builds several vertical pumps entirely in thermoplastic, with no metal parts in contact with the pumped liquid:
The VSK vertical pump is made of PP, PVC or PE for temperatures up to 80 °C. Its cantilever motor shaft has no connections and no shaft guide, which keeps maintenance very simple.
The VGA vertical pump is available in PP, PVC or PVDF for temperatures up to 90 °C, with a ceramic bush guiding the shaft end.
The VL/VLK vertical pump has a mechanical support with aluminium lantern and bearing, an elastic coupling between motor and pump and a ceramic guide bush. Above 2000 mm length it uses a double ceramic guide, which makes it the model for deep tanks.
The vertical range also handles liquids carrying solids or with moderate abrasiveness, which is common in neutralisation pits and spent plating baths.
When large volumes of corrosive liquid have to be recirculated at low head, for instance on a scrubber or during bulk decanting, the EVFA-N external vertical flushed pump is worth considering. Built in polypropylene, it runs with a low-speed motor (1450 rpm) suited to continuous duty, and its mechanical seals are flushed with clean water so they stay in good condition even with very aggressive liquids. A single-seal version without external flushing is also available.
Transfer and recirculation: horizontal centrifugal pumps
If the pump must sit outside the tank, for example to feed several users from one storage tank or to draw from a closed vessel under flooded suction, a horizontal centrifugal pump is used. The key decision is how the shaft is sealed.
The HTM magnetic drive pump, in PP or PVDF for temperatures up to 90 °C, has no mechanical seal at all. Torque reaches the impeller through a magnetic coupling across a sealed separator, so there is no dynamic seal to wear and leak. It is the natural choice for hazardous chemicals where no emission is acceptable; our guide to magnetic drive pumps covers the trade-offs in detail.
The PMC-1 and PMC-2 horizontal pumps use a mechanical seal, single or double flushed; the PMC-2 is a close-coupled design for high flow rates. A double flushed seal puts a barrier between the process fluid and the surroundings.
Dosing and flow control
Accurate dosing is normally done with positive displacement metering pumps (diaphragm or piston), which deliver a fixed volume per stroke and are adjusted by stroke length or frequency. For larger, less critical flows, a centrifugal pump on a variable speed drive can do the job, with the control loop closed on a flow meter or directly on the process measurement, such as pH.
Whatever the technology, three points matter when dosing acids: chemical compatibility of the pump head and check valves, stable delivery across the range of back-pressures, and a pressure relief valve on the discharge. The metering pump itself is selected project by project, according to the chemical, the flow range and the injection point.
Tanks and make-up vessels
The tank is the largest item in most systems. Nuova Darimpianti manufactures polypropylene tanks reinforced with steel frames, including large-capacity units, intended for containing highly corrosive liquids.
When a chemical has to be diluted, dissolved or kept uniform, the make-up tank needs an agitator. Nuova Darimpianti’s mixers for corrosive environments are used in polyelectrolyte preparation, flocculation, neutralisation and physical-chemical water treatment plants, among other duties.
Valves, pipework and instruments
A dependable system needs at least:
isolation valves on both sides of each pump, so it can be taken out of service safely;
check valves on the discharge and, on dosing lines, back-pressure and relief valves;
level indication or transmitters on each tank, with a low-level alarm to protect pumps from running dry and a high-level alarm to prevent overfilling;
pressure gauges fitted with diaphragm seals, so the corrosive fluid never reaches the instrument;
pipework and fittings in the same thermoplastic as the pump, or another compatible material, properly supported and allowing for thermal expansion.
Matching materials to the chemical
Chemical compatibility comes first. Polypropylene (PP), PVC and PVDF are the three thermoplastics found most often in dosing and transfer systems for corrosive fluids, and each has its own operating window. The table below gives common general guidance; final selection must always take concentration, temperature and any oxidisers or impurities into account.
Chemical
Materials usually suitable
Design notes
Hydrochloric acid
PP, PVC, PVDF
Fumes readily: pay attention to vapour seals and tank venting
Dilute sulphuric acid
PP, PVC
Consider PVDF at higher concentrations
Concentrated sulphuric acid
PVDF
Dilution releases a lot of heat: design the mixing step carefully
Sodium hydroxide (caustic soda)
PP
PVDF is not always suitable with hot strong alkalis: check case by case
Sodium hypochlorite
PVC, PVDF
Oxidising: check elastomer compatibility
Ferric chloride, polyelectrolytes
PP, PVC
Typical in water treatment; watch for crystallisation
Nitric acid
PVDF
Strong oxidiser: polyolefins are limited at higher concentrations
O-rings and gaskets deserve the same care. As a rule of thumb, FPM suits many acids, EPDM suits alkalis, and PTFE is the safest all-round choice when the chemical changes or compatibility is uncertain.
Designing out leaks and exposure
Safety is far cheaper to build in at the design stage than to retrofit. The principles are straightforward.
Fewer leak points. Every flange, fitting and seal is a potential leak. Vertical immersion pumps eliminate the suction line; magnetic drive pumps eliminate the mechanical seal. Where a seal is unavoidable, a double flushed seal adds a second line of defence.
Secondary containment. Tanks and pumps should stand in a bund sized for the largest tank, made of or lined with a compatible material. For particularly hazardous chemicals, double-wall tanks with interstitial leak monitoring are common practice. Exact requirements depend on local regulations and on how the substance is classified.
Pump protection. Low-level alarms, dry-running protection and relief valves on positive displacement circuits prevent the most serious failures. A pump damaged by running dry is often where a leak starts.
Fume control. Hydrochloric acid, nitric acid and many plating baths release corrosive and toxic vapours. Tank vents and extraction hoods should be ducted to an abatement system. Nuova Darimpianti builds static-bed and floating-bed abatement scrubbers, from design through to installation.
Sizing: the data you need
Collect this information before requesting a quotation:
Chemical and concentration, with the safety data sheet, any solids or crystals, and viscosity.
Temperature: minimum, normal and maximum.
Flow rate for withdrawal or transfer, and for dosing the turndown range required.
Head: elevation differences, pipe length and diameter, pressure at the injection point. Our guide to pump head and flow calculation walks through the method.
Tank geometry: depth, minimum draw-off level, nozzle arrangement. This sets the immersion length of a vertical pump.
Duty: continuous or intermittent, number of starts per hour, need for a standby pump.
Installation: indoor or outdoor, hazardous area classification, available footprint, power supply.
A common mistake is oversizing “to be safe”. In transfer duty this pushes the pump away from its best efficiency point, with more vibration and faster wear. In dosing it leaves the metering pump running near the bottom of its range, where accuracy is poorest.
Typical applications
Industry
What the system does
Typical components
Water and wastewater treatment
pH correction, flocculation, neutralisation
Make-up tanks with agitators, dosing of acids, alkalis and polyelectrolyte
Electroplating and surface finishing
Bath top-up and recirculation, transfer to effluent treatment
Vertical immersion pumps, magnetic drive pumps, filters
Chemical processing
Reagent storage and transfer, reactor feed
PP tanks, horizontal pumps with double seals or magnetic drive
Air pollution control
Recirculating scrubbing liquor, reagent dosing
High-flow, low-head pumps, dosing of neutralising agent
How Nuova Darimpianti builds custom systems
Alongside individual components, Nuova Darimpianti designs and builds complete skid-mounted plants for treating chemicals and water. Each skid is designed to the customer’s specification, on a stainless steel, painted iron or plastic-coated frame, and comes complete with pumps, tanks, agitators, filters, heat exchangers and pipework, with an electrical control panel on request. Because the system arrives pre-assembled, site work is reduced to a few connections.
Projects start in the in-house engineering office, which takes them from specification to construction, including systems for conveying and pumping aggressive and hazardous products. With 3- and 5-axis machining centres, lathes and milling machines, pumps, agitators and custom parts are machined from solid thermoplastic.
The wider special equipment range covers PP, PE, PVDF and PVC heat exchangers, filter units, oil separators and abatement scrubbers. Once the system is running, the in-house workshop provides routine and extraordinary maintenance on the pumps, agitators and parts supplied.
Frequently asked questions
What is the difference between a transfer system and a dosing system?
A transfer system moves liquid from one tank, pit or drum to another point, and its main requirement is flow. A dosing system injects a controlled amount of chemical into a process, and its main requirement is accuracy. In most plants the two are linked: a transfer pump fills a day tank, and the metering pump draws from it.
When should I use a vertical pump to withdraw chemicals from a tank?
Whenever you are drawing from an open-top tank or pit. A vertical pump works with its casing submerged, needs no priming and has no suction line, which reduces both cavitation risk and the number of leak points. Models such as VSK, VGA and VL are chosen according to tank depth, chemical and temperature.
Which material is best for dosing sulphuric acid?
It depends on concentration and temperature. PP and PVC are commonly used for dilute solutions, while PVDF is generally the safer choice for concentrated acid. Elastomers should be checked just as carefully as the pump body.
How do I prevent leaks in an acid transfer system?
Reduce the number of leak points (vertical pumps, magnetic drive pumps, double flushed seals), install tanks and pumps inside a bund, protect pumps from dry running with level alarms, and fit isolation valves so maintenance can be done safely.
Does Nuova Darimpianti supply complete systems or only components?
Both. Pumps, agitators, tanks and other components are available individually, and the company also designs and builds complete skid-mounted plants for chemical and water treatment, with an electrical panel on request.
Conclusion
Chemical dosing and transfer systems for corrosive fluids work best when every decision starts from the chemical: wetted materials, pump and seal type, containment and fume handling. Sourcing pumps, tanks, agitators and skid assembly from a single supplier also cuts down the interfaces you have to manage.
Planning a new chemical dosing or transfer system, or upgrading an existing one? The engineering team at Nuova Darimpianti can help you select pumps and materials and design the complete installation. Contact us for a no-obligation technical consultation.
The electroplating industry is one of the most aggressive environments for any mechanical component immersed in a treatment tank. Chromic acid solutions at 60°C, pH-controlled nickel plating baths, pickling solutions with hydrochloric and hydrofluoric acid, hot alkaline degreasing baths: each tank presents a different combination of chemical aggressiveness, temperature and mixing requirements.
An inadequate agitator in an electroplating tank does not simply perform poorly — it compromises the quality of the electrodeposit. Insufficient mixing causes non-uniform ion distribution, hot and cold zones in the tank, accumulation of contaminating metal ions near the cathode, and surface defects on the workpiece (porosity, burning, coating delamination).
This guide analyses the specific agitation requirements for each stage of the electroplating process and explains how to select the correct agitator for every type of bath.
Why agitation is critical in electroplating processes
In an electroplating bath, metal deposition occurs through electrochemical reduction of metal ions on the cathode surface (the workpiece to be coated). Deposit quality depends directly on three factors that agitation controls.
Uniform ion distribution
During deposition, metal ions are consumed near the cathode, creating a depleted zone (diffusion boundary layer). If the solution is not adequately agitated, the ionic concentration near the workpiece drops below the critical level and the deposit becomes porous, rough or non-uniform. Agitation constantly renews the boundary layer, maintaining uniform ionic concentration across the entire workpiece surface.
Temperature uniformity
Many electroplating baths operate at controlled temperatures: chrome plating at 50–60°C, nickel plating at 45–55°C, alkaline zinc at 25–35°C. Heating elements or coils create thermal gradients that, without agitation, can reach 5–10°C between different zones of the tank. This non-uniformity causes differences in deposit thickness, aesthetic defects and variations in coating mechanical properties. The agitator maintains temperature uniformity within ±1–2°C.
Gas bubble removal
During electrolysis, hydrogen gas evolves at the cathode. If hydrogen bubbles adhere to the workpiece surface, they prevent metal deposition at those points, creating porosity (pitting). Agitation promotes bubble detachment and removal, improving the surface quality of the deposit.
The effect on cathode efficiency
Agitation has a direct impact on process efficiency. In a chrome plating bath, cathode efficiency with agitation reaches 70–90%, while without agitation it drops to 50–60%. This means that for the same treatment time, the agitated workpiece receives a significantly thicker and more uniform deposit.
Electroplating baths: specific requirements for each treatment type
Each stage of the electroplating cycle has different agitation needs. Let us examine the main ones.
Alkaline degreasing
Degreasing is the first stage of the cycle and uses strongly alkaline solutions (NaOH 30–50 g/l, carbonates, phosphates, surfactants) at temperatures of 50–80°C. Agitation must be vigorous to promote detachment of organic contaminants from the workpiece surface, keep surfactants in emulsion and ensure uniform cleaning across the entire surface.
For this stage, a high-speed EV series agitator with a three-blade marine propeller impeller in PP is the standard choice. The high speed generates the turbulence needed to “strip” oily residues from the metal surface.
Acid pickling
Pickling removes oxides and scale from the surface through immersion in strong acids: 10–20% hydrochloric acid (the most common), 10–25% sulfuric acid, or hydrochloric/hydrofluoric acid blends for stainless steels.
Agitation must be moderate: sufficient to maintain uniform acid concentration and remove reaction products (metal salts) from the surface, but not so violent as to cause excessive base metal removal. The EVR series with pitched blade impeller at low speed (50–150 rpm) is ideal: it generates recirculation without excessive turbulence.
For baths with hydrofluoric acid, the material must be PVDF. For dilute hydrochloric and sulfuric acid, PP is adequate.
Alkaline zinc bath
Alkaline zinc plating uses sodium zincate solutions in a strongly alkaline environment (NaOH 80–140 g/l) at ambient or slightly heated temperature (25–35°C). Agitation must be gentle and uniform to avoid localised turbulence that would cause non-uniform deposits.
A low-speed EVR or KVRL series agitator at 30–80 rpm with PP pitched blade impeller is ideal. PP has excellent resistance to caustic soda, even concentrated — one of the few applications where PP outperforms PVDF.
Nickel bath (Watts)
The Watts bath (nickel sulfate, nickel chloride, boric acid) operates at 45–55°C and pH 3.5–4.5. Agitation must be uniform and low-turbulence to prevent air incorporation and ensure a bright, pit-free deposit.
The EVR series at 40–100 rpm with PP impeller is the typical configuration. For electroless nickel baths that operate at 85–90°C with more aggressive pH, PVDF offers greater reliability.
Chrome plating bath
Chrome plating is the most critical electroplating process from both the agitation and materials standpoint. The bath contains chromic acid (CrO₃ 200–400 g/l) and sulfuric acid as catalyst, at temperatures of 50–60°C.
Chromic acid is a strong oxidiser that attacks both PP and PVC. PVDF is the only adequate thermoplastic material for agitators immersed in chrome plating baths.
Agitation must be moderate and uniform: sufficient to maintain homogeneous temperature and constant ion distribution, but without excessive turbulence that would promote evaporation of chromium compounds (an environmental and health concern). The EVR or KVRL series with PVDF impeller at 30–60 rpm is the optimal configuration.
Acid copper bath
Acid copper plating (copper sulfate in sulfuric acid) operates at ambient temperature with H₂SO₄ concentrations of 5–10%. Agitation must be vigorous near the cathodes to uniformise ion distribution, especially on workpieces with complex geometries (holes, recesses, corners).
The EV series with PP impeller at medium-high speed (300–800 rpm) provides the turbulent flow needed. For plants with large tanks, side-entry agitators from the LVO series may be preferable.
Rinsing and washing
Rinse tanks between process stages require vigorous agitation to rapidly remove chemical drag-out from the workpiece surface. High-speed EV series in PP, with the possibility of multiple installations for large tanks.
Installation configurations for electroplating tanks
Electroplating tanks have specific geometries (typically rectangular, long and narrow) that require particular installation solutions.
Top-entry installation
Top-entry installation is the most common for small and medium tanks. The agitator is mounted on the tank rim with a bracket support. The shaft descends vertically into the solution with the impeller positioned in the lower third of the tank.
For electroplating tanks, Nuova Darimpianti offers the EVL and EVRL series with extended shafts, specifically designed to reach the bottom of deep tanks without requiring intermediate guides.
Side-entry installation
For long tanks where a single top-entry agitator cannot guarantee uniformity along the entire length, side-entry installation (LVO or LRO series) generates a helical flow involving the entire volume. This configuration is particularly effective for electroplating lines with tanks 2–5 metres in length.
Multiple installation
For very large tanks or processes requiring particularly uniform agitation, multiple agitators can be installed on the same tank, distributed evenly along the length. In this case, it is important that the impellers generate complementary (not opposing) flows to avoid zones of excessive turbulence or dead zones.
Fume resistance: an often-overlooked aspect
In hot electroplating tanks, the zone immediately above the liquid level is exposed to concentrated acid fumes and vapours. The agitator shaft passes through this zone and suffers chemical attack that is different from — and often more aggressive than — the attack in the solution.
Chromic acid fumes, for example, attack PP even when the solution below would not (because the fumes are more concentrated and oxidising). For this reason, in chrome plating tanks it is advisable to use PVDF also for the exposed portion of the shaft, or to provide a protective sleeve in the liquid-vapour interface zone.
Agitator maintenance in electroplating environments
The electroplating environment is particularly aggressive for maintenance. Here are the recommended practices.
The impeller and shaft should be visually inspected every 3–6 months for signs of chemical attack (whitening, surface roughness, swelling). Bath concentration and temperature must be constantly monitored: a concentration drift can shift the fluid outside the material’s compatibility zone. Bearings and seals (in gear-reducer versions) must be protected from acid vapours with bellows or sleeves.
Thanks to solid-block CNC machining, Nuova Darimpianti components have no internal stresses that could accelerate chemical degradation: this translates to longer service life compared to moulded components, especially in cyclic environments (tanks heated and cooled daily).
Frequently asked questions
What agitation speed is needed for an electroplating tank?
It depends on the bath type. For chrome and nickel plating, low speeds (30–100 rpm) with pitched blade impellers are ideal to avoid excessive turbulence. For degreasing and rinsing, higher speeds (300–800 rpm) with propeller impellers promote mechanical cleaning. The guiding principle is: deposition baths → low speed; preparation baths → high speed.
Can I use compressed air instead of a mechanical agitator?
Air agitation is a traditional alternative, but has disadvantages: it introduces oxygen into the bath (problematic for many processes), creates acid mists above the tank, does not allow precise control of mixing intensity, and has lower energy efficiency. Mechanical agitators offer more precise control and better efficiency, and are preferred in modern plants.
Which material should I use for an agitator in a chrome plating tank?
PVDF is the only adequate thermoplastic material for chrome plating baths. Chromic acid is a strong oxidiser that attacks both PP and PVC. PVDF resists chromic acid at all concentrations and operating temperatures of chrome plating (50–60°C).
Can the agitator damage workpieces in the tank?
If the impeller is too close to the workpieces hung on the cathode frame, excessive flow can cause non-uniform deposits on exposed edges (the “dog bone” effect). The impeller should be positioned at least 15–20 cm from the workpieces, in the lower third of the tank, where it generates circulation without directly impinging on the cathode surfaces.
Does Nuova Darimpianti supply agitators for complete electroplating lines?
Yes. Nuova Darimpianti designs agitation solutions for the entire electroplating line: degreasing, pickling, deposition baths, rinses and post-deposition treatments. Each tank is individually analysed for size, fluid, temperature and process objective, with personalised selection of series, material and speed.
The right agitator for every stage of the electroplating cycle
The quality of an electroplating treatment depends on many factors, but agitation is one that is too often underestimated. A correctly sized agitator built from the right material improves deposit uniformity, reduces rejects, increases cathode efficiency and extends bath life.
Nuova Darimpianti manufactures high-speed agitators (EV, EVK, EVL, KVL series) and low-speed agitators (EVR, EVRK, EVRL, KVRL series) in PP, PVC and PVDF specifically designed for the electroplating and surface treatment industry. Every component is machined from solid blocks on CNC centres to guarantee maximum chemical resistance and durability even in the most aggressive baths.
Planning a new electroplating line or looking to improve agitation in existing tanks? Contact Nuova Darimpianti’s engineering team for personalised advice.
Transferring corrosive liquids from drums, IBC totes and industrial containers is a daily operation in every chemical plant, electroplating facility and water treatment works. It is also one of the most hazardous operations when performed without the correct equipment: tilting a 200-litre drum of sulfuric acid is dangerous for operators and can cause spills with severe environmental and legal consequences.
Drum transfer pumps solve the problem at its source: they allow the drum contents to be transferred in a controlled, safe manner without manual handling of the container. But not all transfer pumps are the same. The choice depends on the fluid type, viscosity, volume to transfer and operating conditions.
This guide analyses the different types of transfer pump available for corrosive fluids, the selection criteria and the solutions offered by Nuova Darimpianti for the safe transfer of industrial acids, bases and solvents.
Why a dedicated transfer pump is essential
Transferring corrosive liquids from containers is not a trivial operation. Here is why an improvised approach is unacceptable.
Operator safety
Manual tilting of 200-litre drums exposes operators to crushing risks, muscular strain and, above all, corrosive liquid splashes. Even a small spill of hydrofluoric acid or concentrated caustic soda can cause severe chemical burns. Transfer pumps eliminate the need to physically move the container: the operator inserts the suction tube into the drum and starts the pump.
Regulatory compliance
EU REACH regulations, CLP classification and national workplace safety legislation require specific operating procedures for handling hazardous chemical substances. The use of transfer pumps made from compatible materials with anti-drip systems is a prevention measure required in the risk assessment of any company that handles acids and bases.
Transfer control
A transfer pump allows precise flow rate control, preventing overdosing in destination tanks. This is particularly important in electroplating bath preparation, reagent dosing in water treatment plants and filling of storage tanks.
Contamination prevention
Gravity transfer via the drum tap exposes the liquid to air and ambient dust. Transfer pumps with closed systems keep the fluid isolated, avoiding contamination — a critical requirement in the pharmaceutical industry and semiconductor manufacturing.
Types of transfer pump for corrosive fluids
Transfer pumps fall into several categories based on operating principle and installation configuration.
Vertical drum pumps
Vertical drum pumps are the most common solution for emptying 200-litre drums and IBC totes. The principle is straightforward: a vertical tube is inserted into the drum through the top bung. Inside the tube sits an impeller or pumping element which, driven by a motor mounted on top, draws liquid from the drum bottom and pushes it towards the outlet.
The advantages of vertical drum pumps include ease of use (insert, switch on, transfer), ability to empty the drum almost completely, minimal footprint and portability.
Plastic drum pumps are available in PP (for dilute acids, bases, saline solutions) and PVDF (for concentrated acids, solvents, oxidising fluids). Suction tube length ranges from 500 mm (for 25-litre cans) to 1,200 mm (for 200-litre drums) and up to 1,500 mm for IBC totes.
Horizontal centrifugal pumps for transfer
For transfers from storage tanks, vessels or large-volume containers, horizontal centrifugal pumps offer higher flow rates and head than drum pumps. In this context, Nuova Darimpianti’s PMC-1 and PMC-2 series are the ideal solution: horizontal centrifugal pumps with single mechanical seal (PMC-1) or double flushed seal (PMC-2), available in PP, PVC and PVDF.
These pumps are designed for continuous or semi-continuous transfer of significant volumes, with flow rates up to tens of cubic metres per hour and head values covering most plant requirements.
Magnetic drive pumps for safe transfer
When the fluid being transferred is highly hazardous (hydrofluoric acid, carcinogenic solvents, toxic reagents), the HTM series magnetic drive pump guarantees zero leakage during transfer. The absence of a mechanical seal eliminates any possibility of dripping, making the transfer operation compliant with the most stringent regulations.
Pneumatic diaphragm pumps (AODD)
Air-operated double diaphragm pumps are an alternative for transferring viscous fluids or fluids with suspended solids. They run on compressed air (no electrical supply required), are self-priming and can run dry without damage. They are particularly suited to ATEX environments where electric motors cannot be used.
The limitations of pneumatic pumps are flow pulsation (transfer is intermittent rather than continuous) and the need for a compressed air supply.
Selection criteria: how to choose the right transfer pump
Transfer pump selection depends on five main factors.
1. Fluid type and chemical compatibility
The first criterion is the compatibility of the pump material with the fluid being transferred. For dilute acids, bases and saline solutions, PP is the standard choice. For concentrated acids, solvents and oxidising fluids, PVDF is required. For sodium hypochlorite, PVC is the preferred material.
Compatibility applies not only to the pump body but to all wetted components: seals (FPM, EPDM or PTFE), suction tube, discharge hose and fittings.
2. Fluid viscosity
Centrifugal pumps (both drum and horizontal) operate optimally with low to medium-viscosity fluids (up to 200–500 cP). For more viscous fluids (heavy oils, resins, pastes), pneumatic diaphragm or progressive cavity pumps are more suitable.
Most industrial acids and bases have viscosity close to water (1–10 cP), so centrifugal pumps are the ideal choice for chemical reagent transfer.
3. Flow rate and volume
For occasional transfers from individual drums, a vertical drum pump with a flow rate of 50–100 litres per minute is sufficient. For transfers from IBC totes or tanks, horizontal centrifugal pumps with higher flow rates are needed. For continuous supply to production lines, pumps must be sized for the process flow requirement.
4. Required head
If the destination tank is at a higher level than the drum, or if the transfer line is long, the pump must provide sufficient head to overcome the height difference and friction losses. Vertical drum pumps have limited head (3–10 metres). Horizontal centrifugal PMC pumps achieve significantly higher head values.
5. Installation environment (ATEX)
In environments with explosion risk (ATEX zones), electric motors must be Ex-certified or replaced with pneumatic drives. Nuova Darimpianti offers versions with pneumatic motors for its pumps and agitators, compliant with regulations for classified environments.
Essential accessories for safe transfer
A transfer pump alone is not sufficient for a safe and controlled operation. Accessories complete the system.
Resistant tubing and fittings
Suction and discharge tubing must be made of material compatible with the fluid. PP tubing, PVDF tubing or flexible PTFE-lined hoses are the standard options. Fittings must ensure leak-tightness and allow quick, secure connection.
Anti-drip systems
At the end of transfer, residual liquid in the suction tube tends to drip during extraction from the drum. Anti-drip systems (check valves, closure caps) prevent spills and contamination of the work area.
Flow meters
For precise dosing operations, a flow meter mounted on the discharge line allows exact control of the transferred volume. Flow meters in PP or PVDF are available for corrosive fluids.
Containment bunds
Regulations require that hazardous substance transfer operations take place over containment bunds capable of holding the entire drum volume in case of accidental spillage.
Typical applications for industrial transfer
Transfer is an operation that crosses many industrial sectors.
Electroplating bath preparation
Preparing electroplating baths requires precise transfer of acids (sulfuric, hydrochloric, chromic) and additives from drums to treatment tanks. PVDF transfer pumps are essential for chromic acid; PP is adequate for dilute acids.
Reagent dosing in water treatment plants
Sodium hypochlorite, sulfuric acid for pH correction, polyelectrolytes: these reagents are supplied in drums or IBC totes and must be transferred to dosing tanks. PVC transfer pumps for hypochlorite, PP for dilute acids.
Storage tank refilling
Transfer from tanker trucks to the plant’s storage tanks requires horizontal centrifugal pumps with high flow rates. Nuova Darimpianti’s PMC-1 and PMC-2 series cover this need with flow rates up to tens of m³/h.
Laboratories and pilot plants
In chemical laboratories and pilot plants, transfer involves small volumes but often highly hazardous fluids. PVDF drum pumps with variable-speed motors allow precise control even at low flow rates.
Pharmaceutical industry
Transferring pure solvents and reagents requires pumps that do not contaminate the fluid. HTM series magnetic drive pumps in PVDF are the standard for these applications, guaranteeing zero contamination and zero leakage.
The Nuova Darimpianti solution for chemical transfer
Nuova Darimpianti offers a complete range of solutions for corrosive fluid transfer, all based on solid-block CNC machining for maximum reliability.
PMC-1 and PMC-2 horizontal centrifugal pumps are ideal for transfers from tanks and IBC totes with high flow rates and head. PMC-1 with single seal for standard fluids, PMC-2 with double flushed seal for hazardous fluids.
HTM magnetic drive pumps are the choice for highly hazardous fluids where zero leakage is a non-negotiable requirement.
VSK and VGA vertical pumps are perfect for direct suction from open tanks and vessels, eliminating the need for priming.
All models are available in PP, PVC and PVDF, with electric or pneumatic motor options for ATEX environments.
Frequently asked questions
Which pump do I need for transferring sulfuric acid from drums?
For dilute sulfuric acid (up to 50%), a PP drum pump is sufficient. For concentrated sulfuric acid (70–98%), PVDF is required. For transfers from IBC totes or larger volumes, a PVDF PMC horizontal centrifugal pump is the most efficient solution.
Can transfer pumps handle viscous fluids?
Centrifugal pumps work well up to 200–500 cP. For more viscous fluids (heavy oils, resins, pastes), pneumatic diaphragm pumps are more suitable. Most industrial acids and bases have very low viscosity and pose no issues.
Is it safe to use a transfer pump in an ATEX zone?
Yes, provided the motor is ATEX-certified or a pneumatic drive is used. Nuova Darimpianti offers pneumatic motor versions for all its pumps, compliant with regulations for explosive atmosphere environments.
How often should a transfer pump for acids be inspected?
Seals and wetted parts should be inspected every 3–6 months, or more frequently for intensive use with concentrated acids. Solid-block CNC-machined pump bodies last significantly longer than moulded components, requiring less frequent replacement.
Can I use the same pump for different acids and bases?
It is technically possible if the material is compatible with all fluids (for example, a PVDF pump can handle both acids and dilute bases). However, to avoid cross-contamination between incompatible fluids, it is good practice to dedicate a pump to each fluid type or to perform a thorough flush between uses.
Safe transfer is an investment, not a cost
A correctly designed transfer system protects operators, satisfies regulations, prevents spills and safeguards product quality. The cost of a transfer pump in adequate material is a fraction of the cost of a chemical accident, environmental remediation or contaminated production batch.
Nuova Darimpianti designs and manufactures pumps for corrosive fluid transfer in PP, PVC and PVDF, all machined from solid blocks on CNC centres. From small drum pumps to centrifugal pumps for storage tank refilling, every solution is sized to the specific requirements of your plant.
Need a solution for safe transfer of acids, bases or solvents in your plant? Contact our engineers for personalised advice.