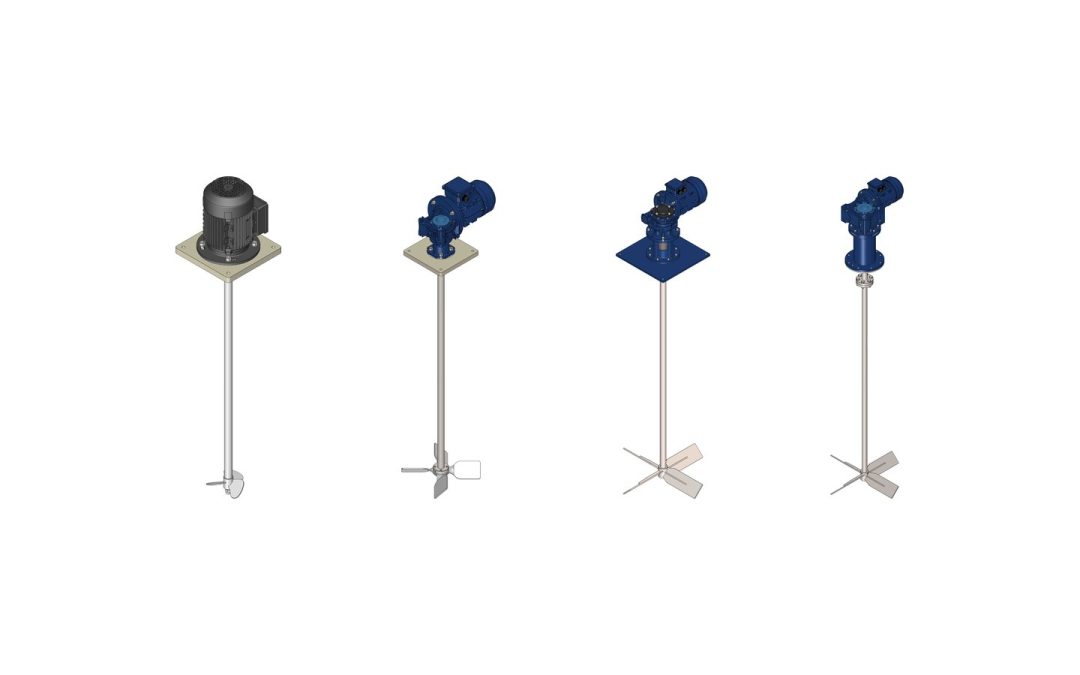
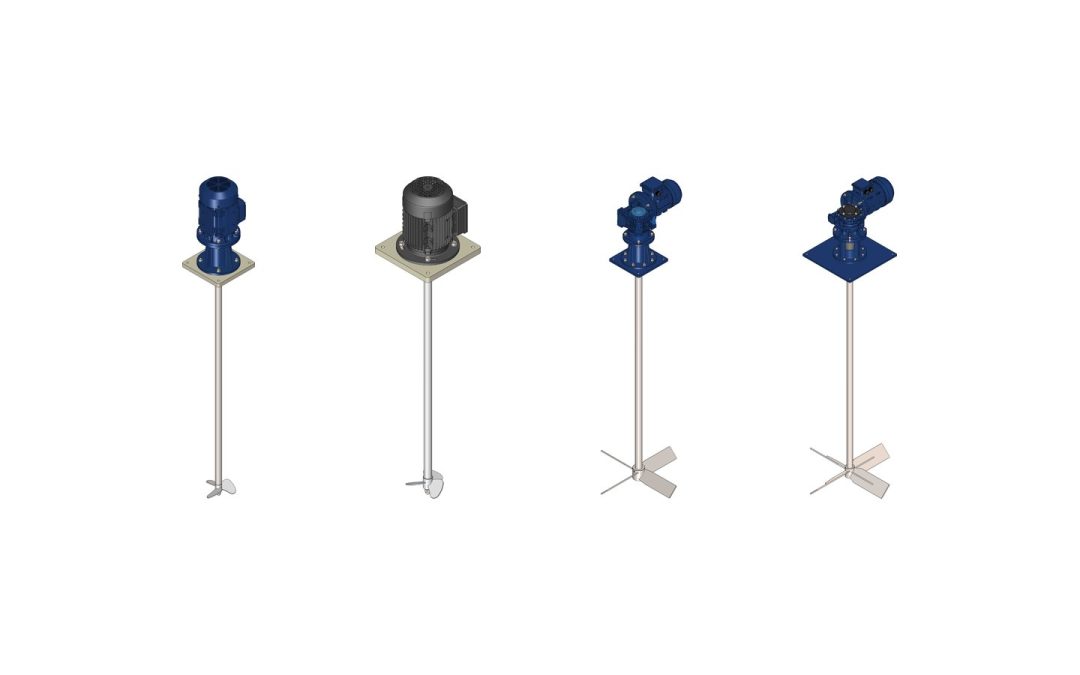
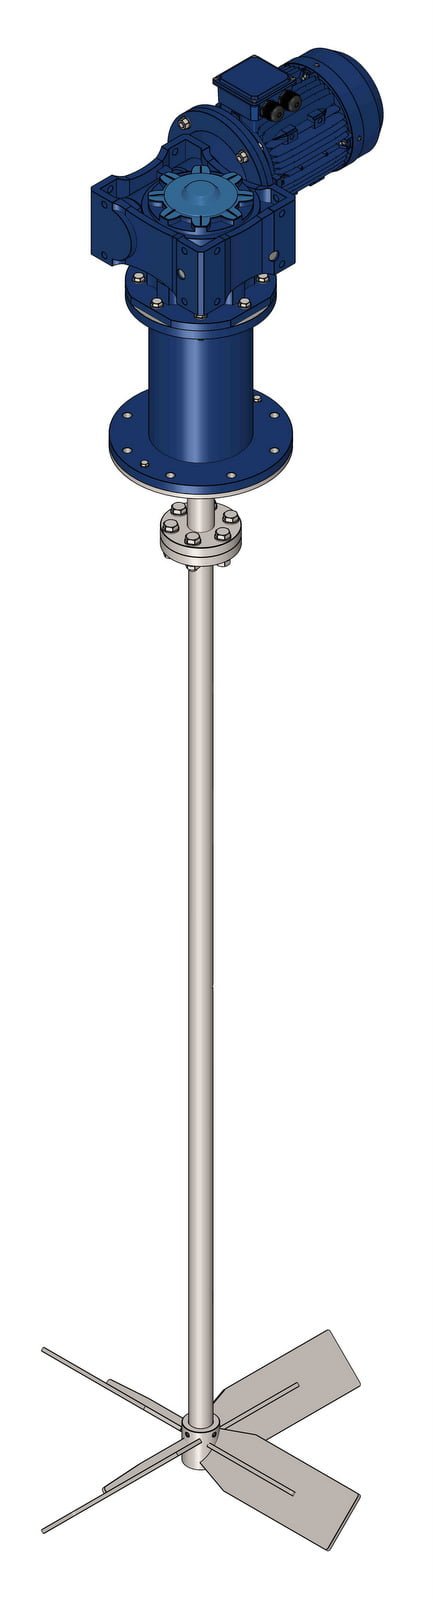
Put two agitators with the same motor and shaft into the same tank and you can still get opposite results. The difference is the impeller. Different agitator impeller types decide how the fluid moves, how much shear reaches droplets, bubbles and agglomerates, and how much motor power becomes useful mixing rather than heat and vortex.
This guide reviews the impellers we fit at Nuova Darimpianti on agitators for corrosive service: marine propeller, Cowles (cowless) disc, Rushton turbine, emulsifier, folding blades, pitched blades, high-flow, anchor and scraper. For each one we cover flow, viscosity, uses and limits. For the full agitator selection process (process objective, Reynolds number, motor), start with how to choose an industrial agitator; here we stay on the impeller.
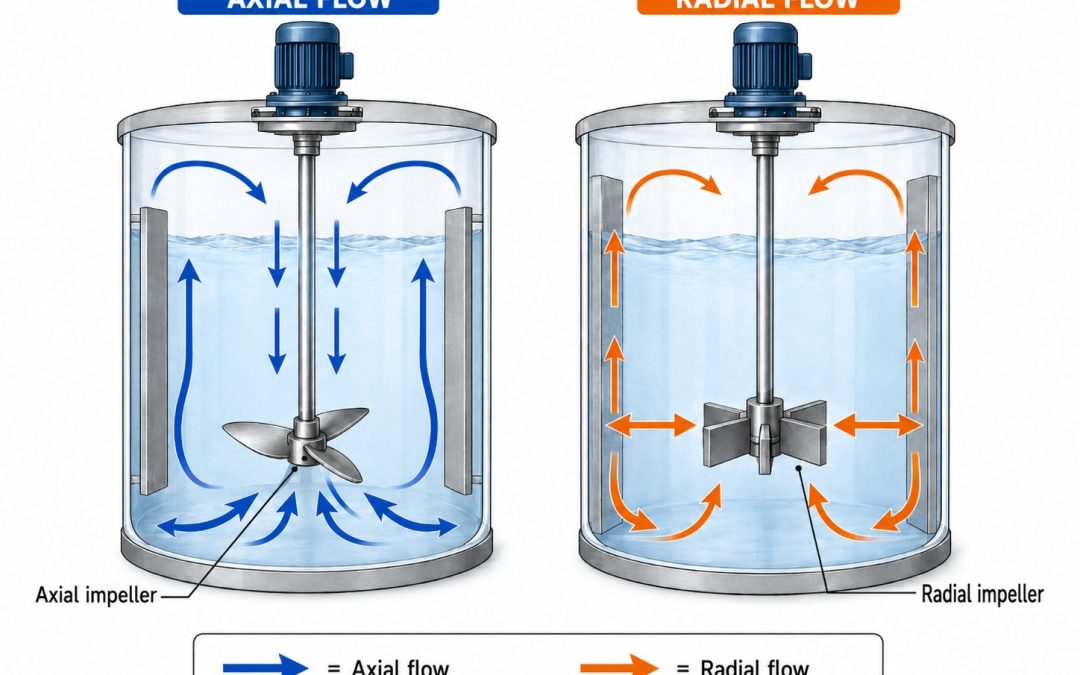
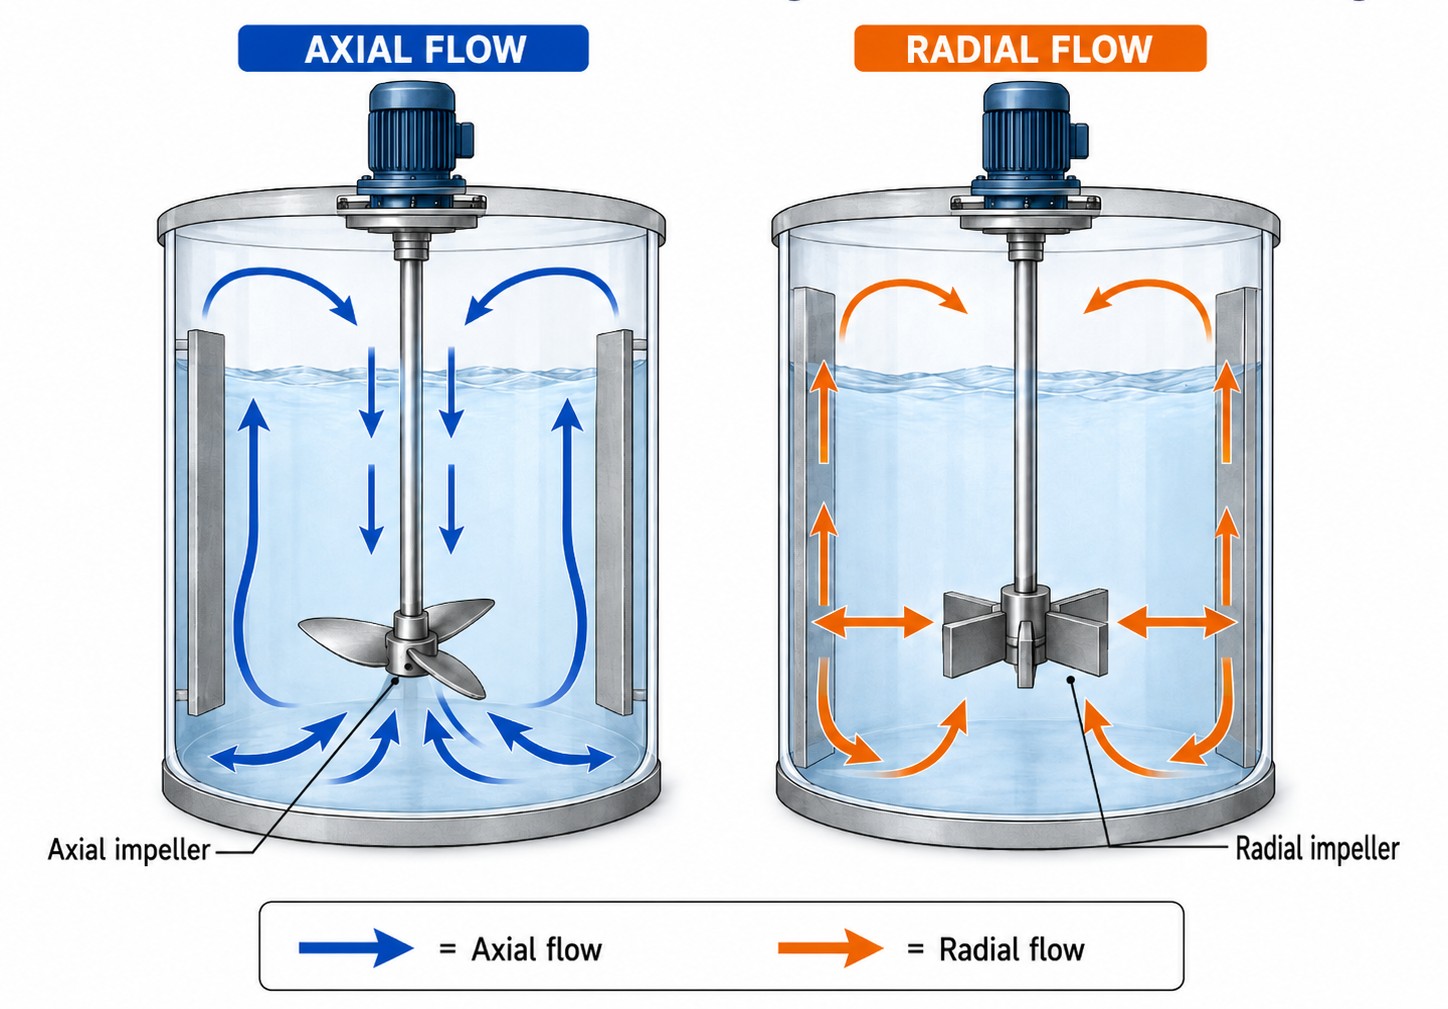
Axial, radial and tangential flow
Every impeller pushes fluid in a dominant direction, and that direction sets the job it does well.
Axial flow
Axial impellers push liquid parallel to the shaft, usually towards the bottom. The jet rises along the walls and returns to the impeller, forming a single loop that sweeps the whole volume. This is the most efficient pattern for blending, keeping solids suspended and evening out temperature with little power. Marine propellers, pitched blades (mixed flow with an axial bias) and high-flow impellers belong here.
Radial flow
Radial impellers discharge fluid towards the walls, creating two loops above and below the impeller. They pump less liquid per kW but concentrate a lot of shear close to the blades: what you need to disperse powders and pigments, break agglomerates, emulsify or break up a gas. Cowles discs, Rushton turbines and emulsifiers are radial.
Tangential flow
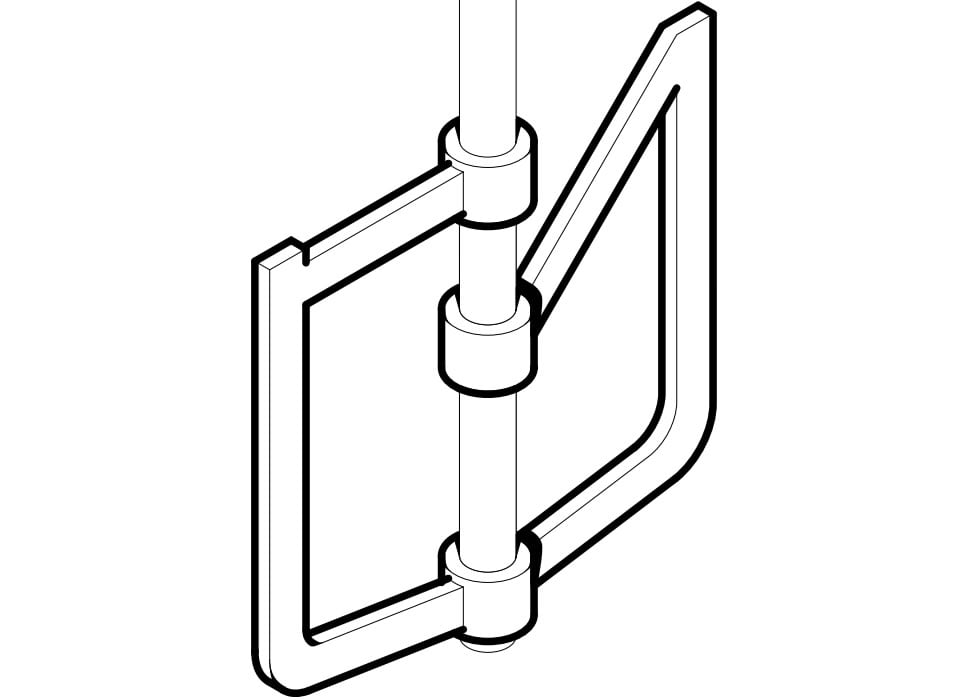
Anchors and scrapers turn slowly with a diameter close to the tank diameter, dragging the fluid round and acting continuously on the wall. You need them when the product is so viscous that a small impeller would only stir a “cavern” of liquid around itself.
In unbaffled cylindrical tanks, fast impellers tend to spin the whole liquid and pull a central vortex. The usual fixes are baffles, off-centre or angled mounting and side-entry agitators. Anchors, by contrast, run without baffles.
Agitator impeller types one by one
Speeds quoted are those on our product datasheets. Viscosity ranges are indicative and should be checked against the real fluid.
Three-blade marine propeller
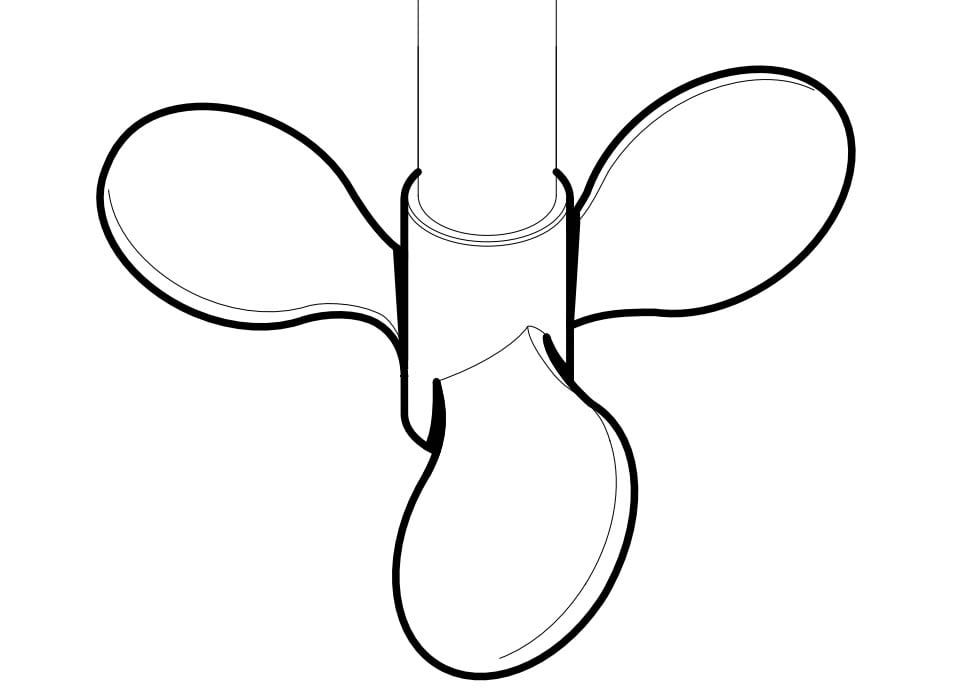
The most common impeller on fast agitators: three helical blades driving liquid towards the bottom with clean axial flow and low power. It runs from 500 to 1,500 rpm and is the standard impeller on the EV and EVK ranges.
Viscosity: low, up to about 2,000-3,000 cP.
Typical uses: diluting and neutralising acids and alkalis, preparing solutions, water treatment.
Strengths: high flow per kW, low vibration.
Limits: little shear; in viscous fluids the flow dies out near the impeller.
Cowles (cowless) disc impeller
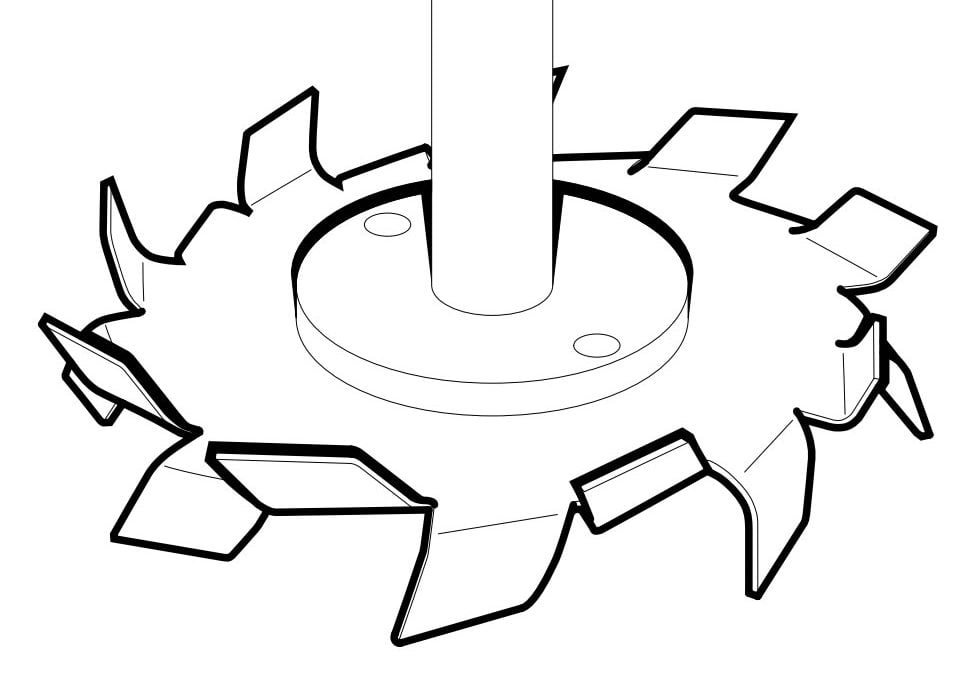
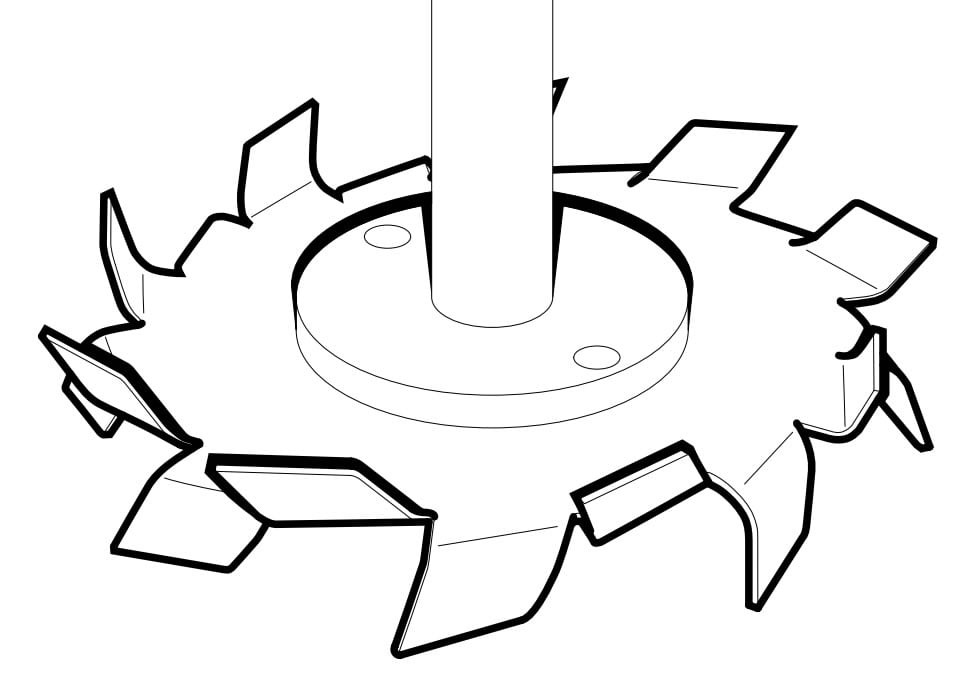
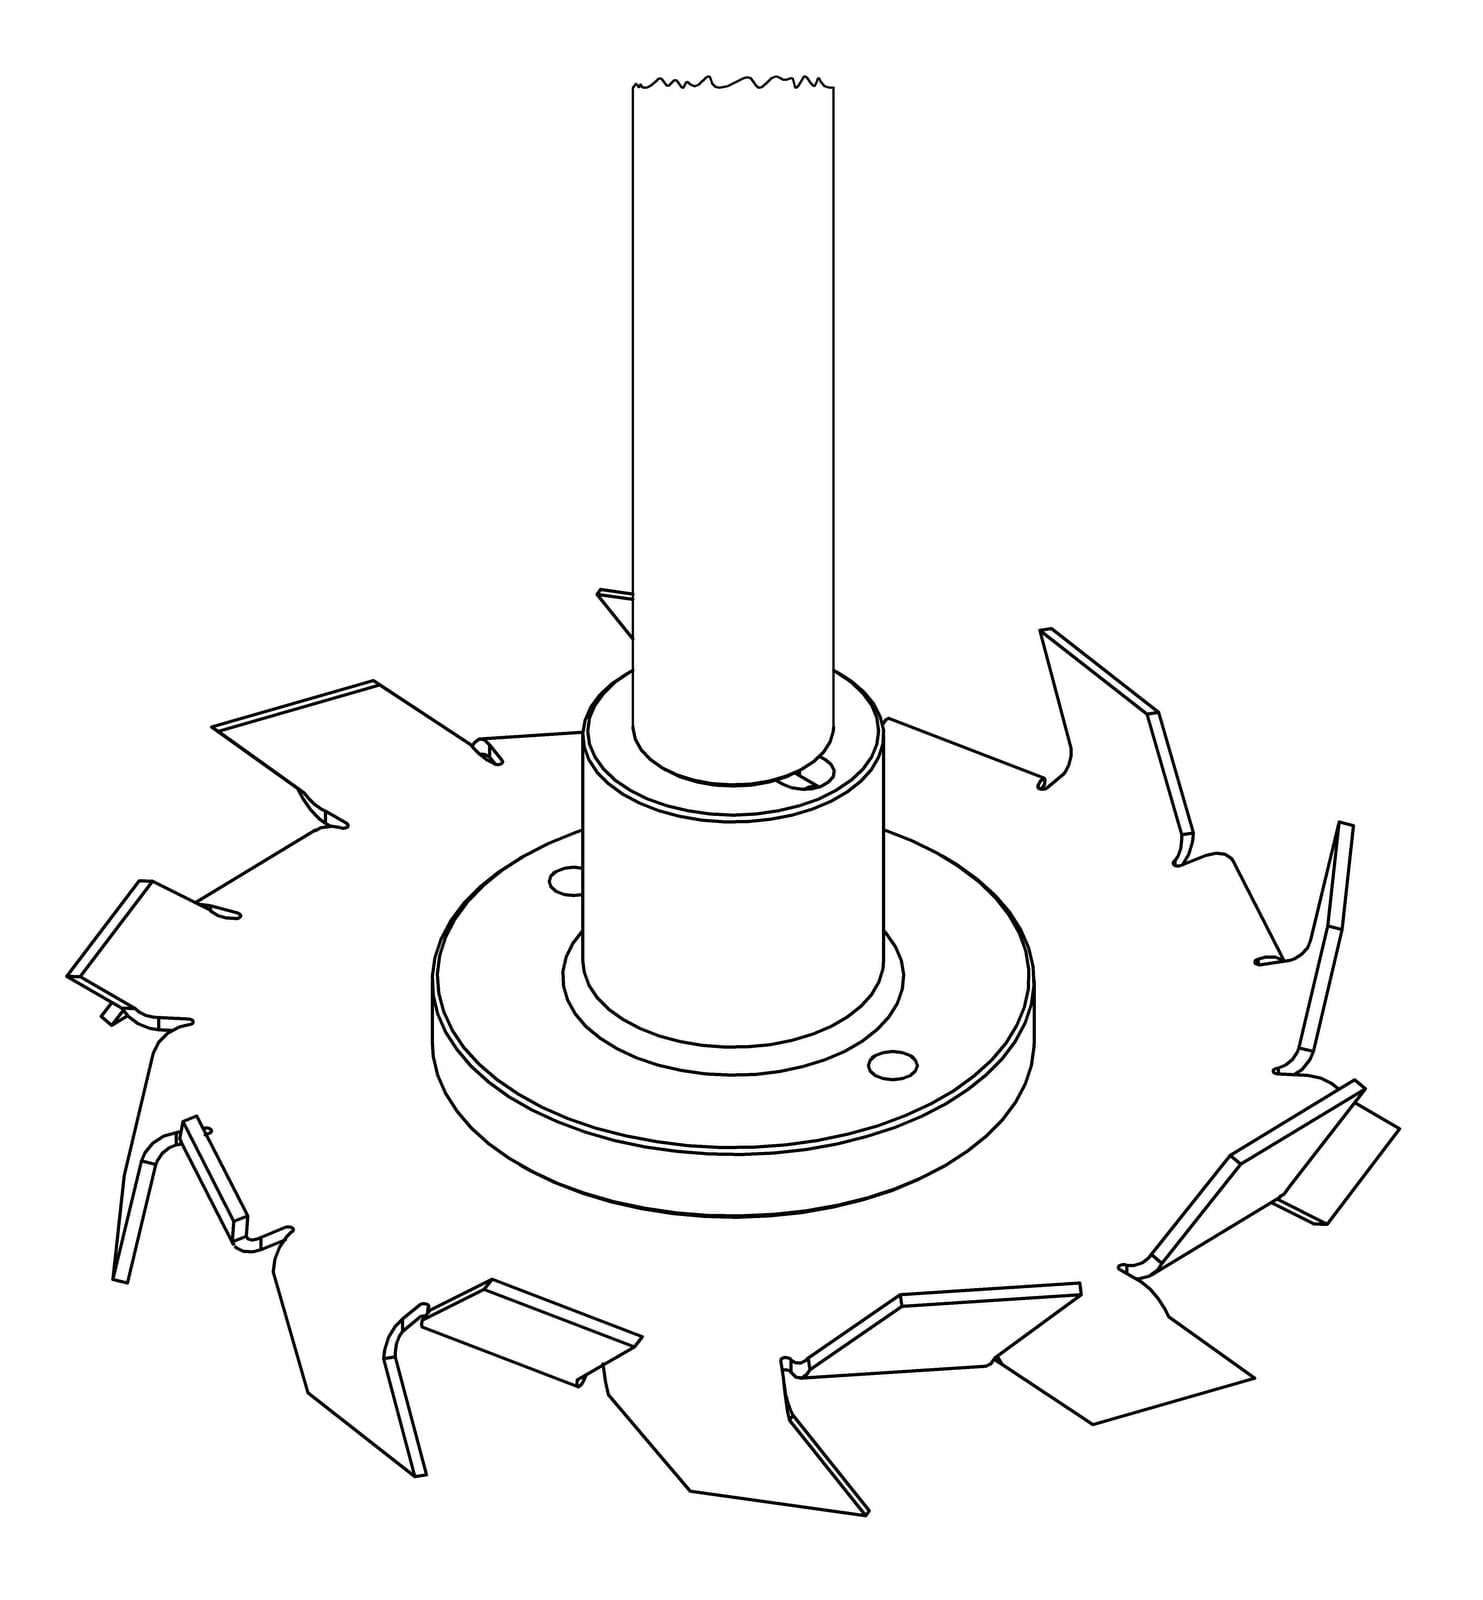
The Cowles impeller, often spelled “cowless” and also called a toothed disc or disperser blade, is a disc with teeth bent alternately up and down. At high speed it creates a very intense shear zone at the rim while product is drawn in from above and below and thrown towards the walls. It has the widest range in our line-up: 300 to 3,000 rpm. In dispersers the disc tip speed matters more than rpm (see sizing below).
Viscosity: from thin liquids to pastes of a few tens of thousands of cP, as long as product keeps flowing back to the disc.
Typical uses: dispersing pigments and fillers in paints and inks, fast powder dissolution, breaking agglomerates.
Strengths: very high shear from a simple, easy-to-clean geometry.
Limits: low pumping, so large tanks need a second circulation impeller; high power draw at top speed.
Straight-blade Rushton turbine
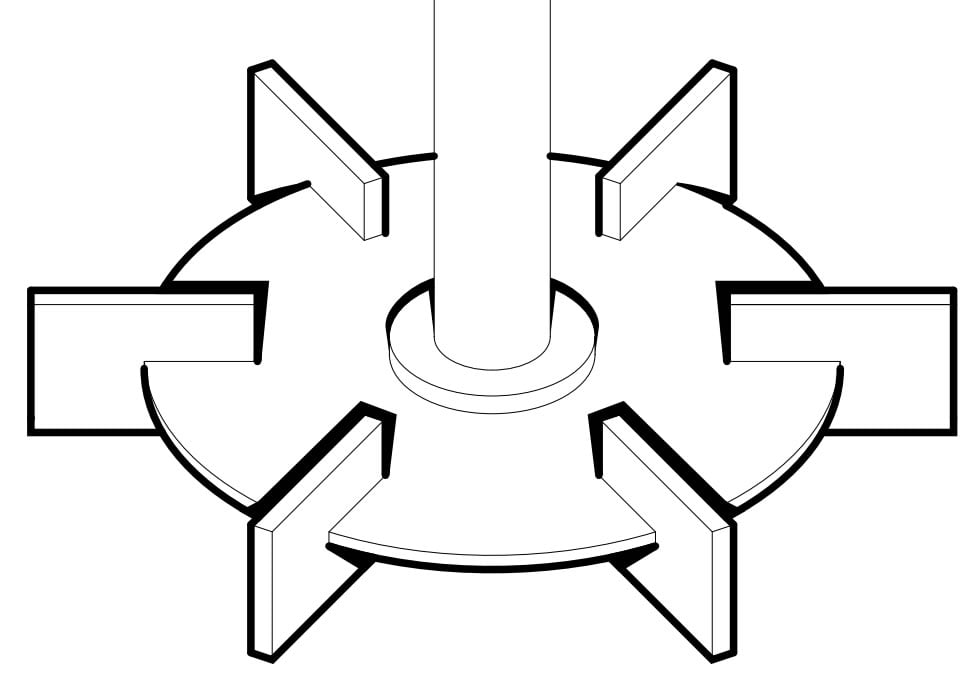
Six flat vertical blades on a disc. The disc stops gas sparged from below escaping up the shaft and forces it through the blades, where it is broken up. It runs from 300 to 1,400 rpm.
Viscosity: low to medium, below about 5,000 cP.
Typical uses: gas-liquid dispersion, reactions needing high mass transfer.
Strengths: high local turbulence, well-documented behaviour.
Limits: high power number; needs baffles; inefficient for plain blending.
Emulsifier impeller
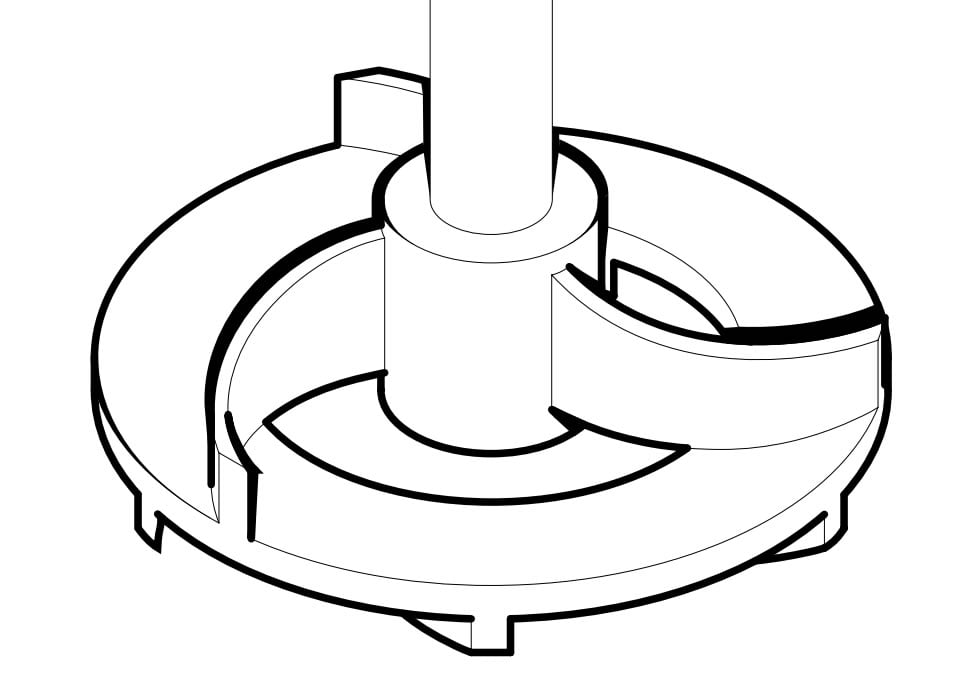
Curved vanes inside a toothed ring: liquid enters at the centre, is accelerated and leaves through the ring, where it is sheared hard and repeatedly. It runs from 500 to 2,000 rpm.
Viscosity: low to medium.
Typical uses: emulsions of immiscible phases, fine and stable dispersions.
Strengths: smaller, more uniform droplets than an open impeller.
Limits: modest circulation; more sensitive to coarse solids.
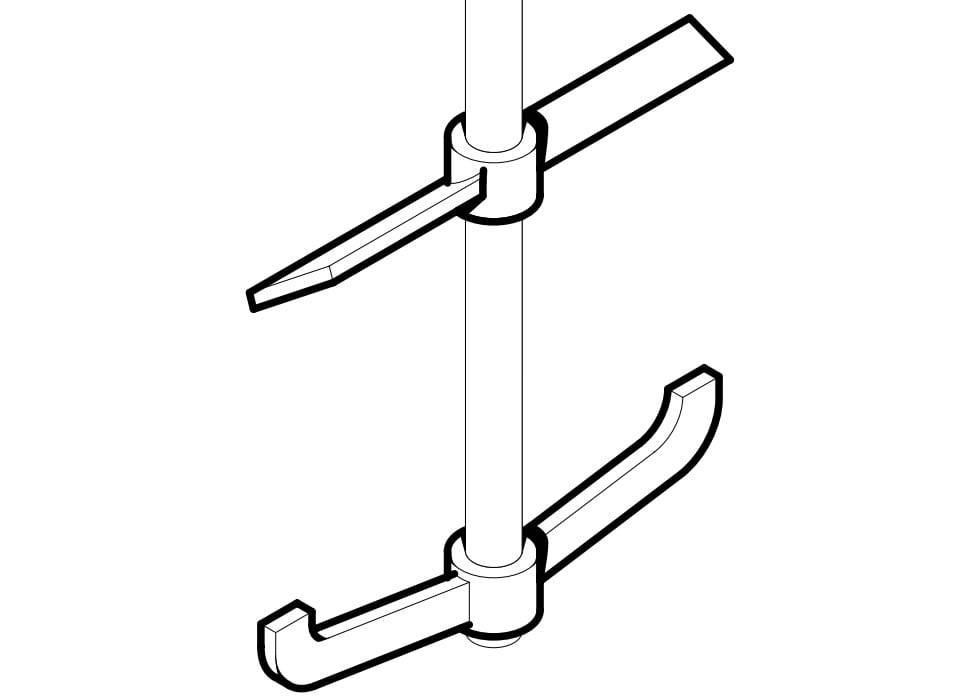
Folding-blade (movable-blade) impellers
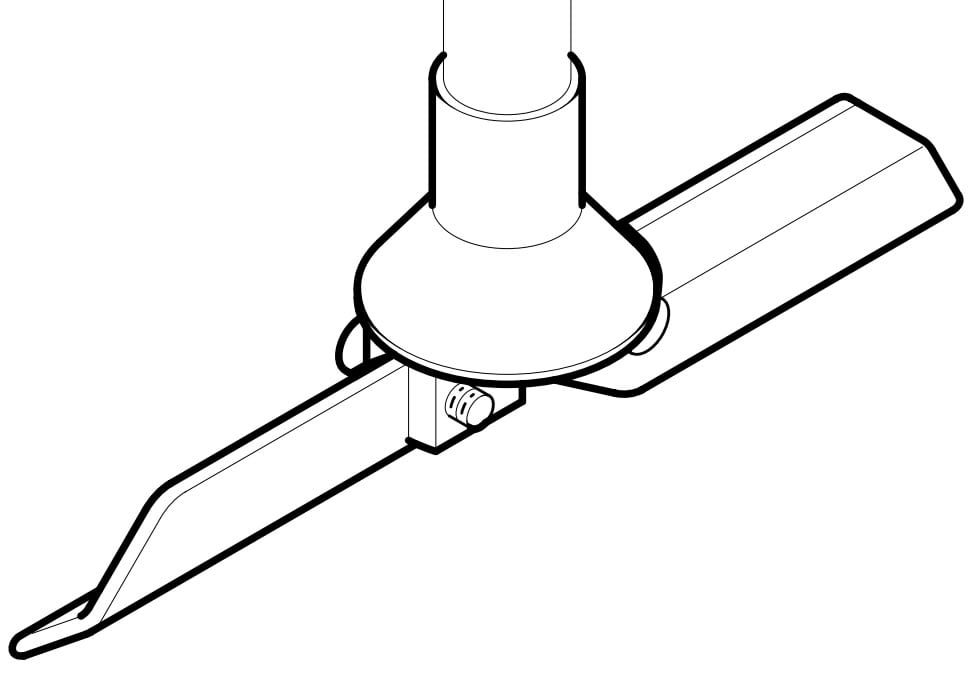
Folding-blade agitators are built for containers with a small opening, such as IBC totes and drums. The blades are pinned to the hub: in the usual arrangement they hang along the shaft when stopped, pass through the filler neck, then swing open as the shaft turns and work at full diameter. Our datasheets list the movable-blade impeller in the fast range (300-1,500 rpm) and, as a four-blade version, in the slow range (up to 400 rpm).
Viscosity: low to medium.
Typical uses: re-mixing additives and reagents in IBCs, re-suspending settled solids.
Strengths: working diameter larger than the opening; one agitator can serve several totes.
Limits: the hinge needs checking with solids-laden or crystallising fluids.
Pitched-blade turbine and modular impeller
Four flat blades set at an angle, usually 45°, give mixed flow with an axial bias. It is the workhorse of slow agitators: the pitched-blade turbine and modular pitched-blade impeller run from 10 to 380 rpm. The four-blade impeller also comes with straight blades when more radial action is needed.
Strengths: versatile; several impellers can be stacked in tall tanks.
Limits: draws more power than a high-flow impeller for the same flow.
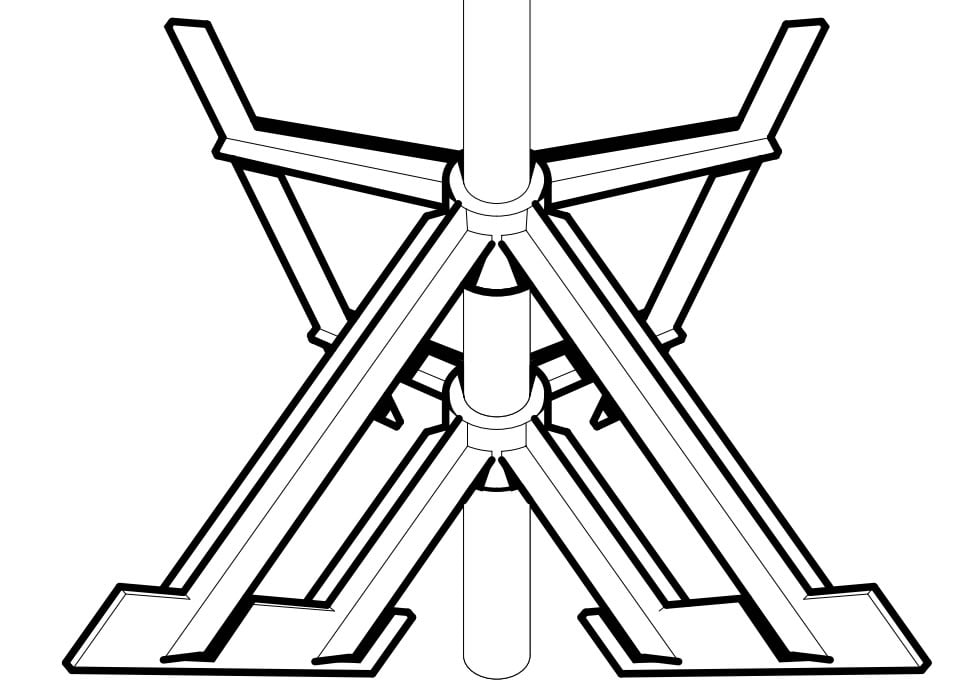
High-flow four-blade impeller
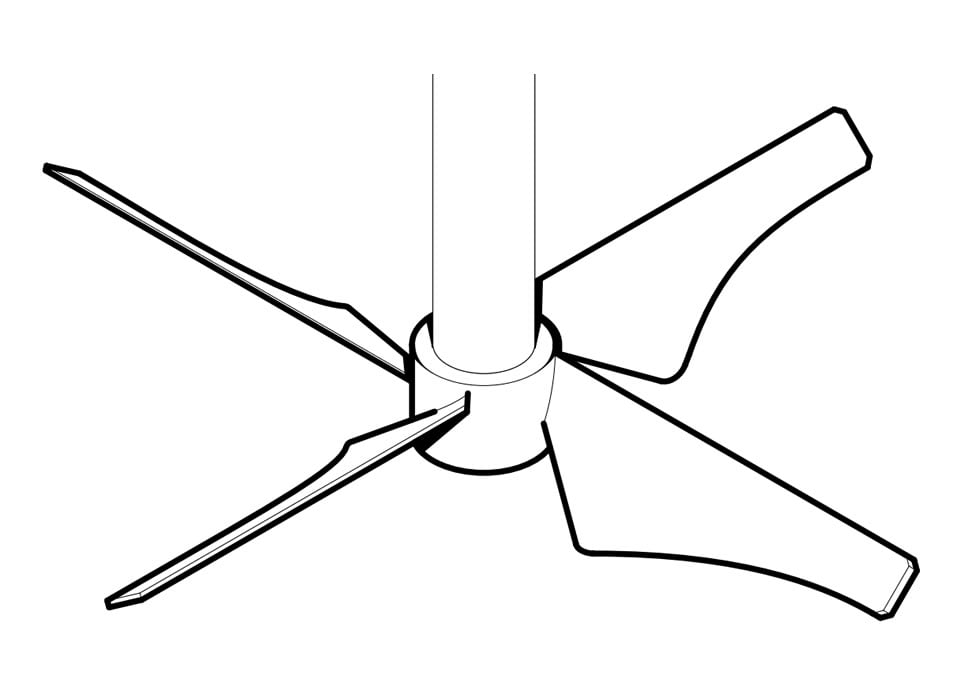
Profiled blades, wide at the root and tapering to the tip, designed to move the most volume with the least shear. It runs from 10 to 380 rpm on the EVRK, EVRL and KVRL ranges and the LRO side-entry mixer.
Viscosity: low, best below about 1,000 cP.
Typical uses: large tanks, solids suspension, flocculation where flocs must not break.
Strengths: low power number, so smaller gear motors.
Limits: loses effectiveness as viscosity rises; unsuited to dispersion.
Anchor impeller: gate anchor and anchor with paddle
The anchor follows the tank profile close to wall and bottom, turns slowly (5-56 rpm on our datasheets) and moves the whole batch by drag. The version with a paddle adds an upper arm that improves vertical turnover, the weak point of a plain anchor.
Strengths: moves the whole volume; improves heat transfer at the wall.
Limits: poor vertical exchange without extra paddles; high torque.
Scraper impeller
The scraper takes the anchor idea to its limit: arms and shoes work almost in contact with bottom and walls, removing product that sticks, settles or crystallises. We design scrapers to order around the tank and the product.
Viscosity: high, or products that build deposits.
Typical uses: fouling products, sludges that compact, wall-heated tanks.
Strengths: clean walls and bottom, steady heat transfer.
Limits: shoe wear; high power and starting torque.
Impeller comparison table
Impeller
Flow
Indicative viscosity
Speed (Nuova Darimpianti datasheets)
Typical applications
Three-blade marine propeller
Axial
Up to 2,000-3,000 cP
500-1,500 rpm
Dilution, neutralisation, water treatment
Cowles (cowless) disc
Radial, very high shear
Thin liquids to pastes
300-3,000 rpm
Pigment dispersion, powder dissolution
Rushton turbine
Radial
Below 5,000 cP
300-1,400 rpm
Gas dispersion, reactions
Emulsifier
Radial, high shear
Low-medium
500-2,000 rpm
Emulsions, fine dispersions
Folding blades
Mixed
Low-medium
300-1,500 rpm (fast); up to 400 rpm (slow)
IBCs, drums, narrow openings
Pitched blade / modular
Mixed, mainly axial
Up to about 10,000 cP
10-380 rpm
Flocculation, polyelectrolyte, plating
High-flow four-blade
Axial
Below about 1,000 cP
10-380 rpm
Large tanks, solids suspension
Anchor (gate / with paddle)
Tangential
5,000 to over 50,000 cP
5-56 rpm
Resins, gels, jacketed tanks
Scraper
Tangential with wall scraping
High or fouling
Custom design
Products that foul or settle
Sizing basics: D/T ratio, tip speed and power number
The D/T ratio
D is the impeller diameter, T the tank diameter. Typical values: 0.2-0.35 for marine propellers, 0.25-0.4 for Cowles discs and Rushton turbines, 0.3-0.5 for pitched-blade and high-flow impellers, 0.9-0.98 for anchors and scrapers. Too small a D/T leaves dead zones; too large, on a fast impeller, sends power soaring.
Tip speed
The velocity of the blade tip:
v = π · D · N / 60
with v in m/s, D in metres and N in rpm. A 150 mm Cowles disc at 3,000 rpm reaches about 23.6 m/s, typical for dispersers; a 1.5 m anchor at 20 rpm about 1.6 m/s. Tip speed is the most direct indicator of shear and the figure to watch on thermoplastic impellers, which tolerate lower tip speeds than steel.
Power number and power draw
In turbulent flow, in a baffled tank:
P = Np · ρ · N³ · D⁵
with P in watts, ρ in kg/m³, N in revolutions per second and D in metres. Np depends on geometry: about 0.3-0.5 for marine propellers and high-flow impellers, 1.2-1.5 for a 45° four-blade turbine, about 5 for a Rushton.
Example: a 0.2 m propeller at 900 rpm (15 rev/s) in water, Np = 0.35: P = 0.35 × 1,000 × 15³ × 0.2⁵ ≈ 380 W. A Rushton of the same size at the same speed takes over 5 kW. Doubling speed multiplies power by 8, doubling diameter by 32, and power scales with density: in concentrated sulphuric acid (about 1,840 kg/m³) the same agitator draws nearly twice as much as in water. The motor is then chosen with a margin over this figure. In laminar flow the formula no longer applies in this form: anchors and scrapers are sized on torque. The link between viscosity and flow regime is covered in fast vs slow agitators.
Impeller materials for corrosive service
Choose the material for the worst product the impeller will see, at the highest temperature. On our fast ranges impellers come in AISI 304-316 stainless steel or in PP, PVC or PVDF; on the slow ranges also in PE-HD, and on the KVRL they can be ebonite-coated.
PP: dilute acids and alkalis, plating baths, water treatment, up to 80-90°C.
PVC: stiff and economical, but limited to 60°C.
PVDF: concentrated acids, strong oxidisers, up to 100-120°C.
AISI 304-316: with compatible fluids, for the highest tip speeds.
Matching impellers to fast, slow and side-entry agitators
Fast agitators. On EV/EV-G and EVK the standard impeller is the three-blade marine propeller. The EVL range, with a single or double bearing lantern, and the KVL also take the straight-blade turbine, emulsifier and Cowles disc: these are the machines to choose when the impeller draws more power or runs at high tip speed.
Slow agitators. The EVR range, with the shaft keyed directly to the gearbox, carries the four-blade impeller with pitched or straight blades; EVRK and EVRL add the high-flow impeller and a lantern for medium and high loads. The KVRL, built for heavy loads, can carry 2 to 4 two-blade or four-blade impellers on one shaft, the answer for tall tanks or variable levels.
Side-entry agitators. The fast LVO takes the propeller, straight-blade turbine, emulsifier or Cowles disc; the slow LRO takes the four-blade impeller with pitched, straight or high-flow blades. Side entry suits large tanks and helps avoid a central vortex.
Frequently asked questions
What is the difference between a Cowles (cowless) impeller and a Rushton turbine?
Both produce radial flow. The Cowles disc concentrates very intense shear at the rim and is designed to disperse powders and pigments at high tip speed. The Rushton has flat blades on a disc, spreads turbulence more evenly and is the classic choice for dispersing gas into a liquid.
What are folding-blade agitators?
Agitators whose blades are hinged at the hub, so they fold to pass through a narrow opening and open as the shaft turns. They are mainly used to mix IBC totes and drums, where a rigid impeller of the required diameter would not fit through the filler neck.
Which impeller should I use for a very viscous fluid?
Above roughly 5,000-10,000 cP, small fast impellers only move the liquid around them. Use an anchor, possibly with an upper paddle, or a scraper if the product sticks to the walls. They run slowly, our anchor from 5 to 56 rpm, with gearboxes sized on torque.
Can I fit more than one impeller on the same shaft?
Yes, it is standard in tall tanks. The KVRL range takes 2 to 4 two-blade or four-blade impellers. Dispersion processes often pair a shear impeller, such as a Cowles disc, with an axial circulation impeller, to be assessed case by case.
Plastic or steel impeller?
It depends on the fluid and the tip speed. With acids, alkalis and oxidisers, PP, PVC and PVDF avoid corrosion; with compatible fluids and very high tip speeds, AISI 304-316 steel gives more mechanical margin. Often the answer is a coated steel shaft with a thermoplastic impeller machined from solid.
Conclusion: start from the flow you need
Choosing between agitator impeller types starts with one question: what has to happen in the tank? For circulation, look at axial impellers (marine propeller, pitched blade, high-flow); for shear, at radial ones (Cowles disc, Rushton, emulsifier); for thick products or fouling walls, at anchors and scrapers. Then check D/T, tip speed and power, and choose the material for the most aggressive fluid.
Choosing an impeller for a new agitator, or replacing one that underperforms? Nuova Darimpianti’s engineering team in Flero (Brescia, Italy) has been designing and building agitators and impellers in PP, PVC, PVDF and stainless steel for corrosive fluids since 1970, including custom designs. Send us your fluid, viscosity, volume and tank geometry: contact us for a no-obligation technical consultation.
The electroplating industry is one of the most aggressive environments for any mechanical component immersed in a treatment tank. Chromic acid solutions at 60°C, pH-controlled nickel plating baths, pickling solutions with hydrochloric and hydrofluoric acid, hot alkaline degreasing baths: each tank presents a different combination of chemical aggressiveness, temperature and mixing requirements.
An inadequate agitator in an electroplating tank does not simply perform poorly — it compromises the quality of the electrodeposit. Insufficient mixing causes non-uniform ion distribution, hot and cold zones in the tank, accumulation of contaminating metal ions near the cathode, and surface defects on the workpiece (porosity, burning, coating delamination).
This guide analyses the specific agitation requirements for each stage of the electroplating process and explains how to select the correct agitator for every type of bath.
Why agitation is critical in electroplating processes
In an electroplating bath, metal deposition occurs through electrochemical reduction of metal ions on the cathode surface (the workpiece to be coated). Deposit quality depends directly on three factors that agitation controls.
Uniform ion distribution
During deposition, metal ions are consumed near the cathode, creating a depleted zone (diffusion boundary layer). If the solution is not adequately agitated, the ionic concentration near the workpiece drops below the critical level and the deposit becomes porous, rough or non-uniform. Agitation constantly renews the boundary layer, maintaining uniform ionic concentration across the entire workpiece surface.
Temperature uniformity
Many electroplating baths operate at controlled temperatures: chrome plating at 50–60°C, nickel plating at 45–55°C, alkaline zinc at 25–35°C. Heating elements or coils create thermal gradients that, without agitation, can reach 5–10°C between different zones of the tank. This non-uniformity causes differences in deposit thickness, aesthetic defects and variations in coating mechanical properties. The agitator maintains temperature uniformity within ±1–2°C.
Gas bubble removal
During electrolysis, hydrogen gas evolves at the cathode. If hydrogen bubbles adhere to the workpiece surface, they prevent metal deposition at those points, creating porosity (pitting). Agitation promotes bubble detachment and removal, improving the surface quality of the deposit.
The effect on cathode efficiency
Agitation has a direct impact on process efficiency. In a chrome plating bath, cathode efficiency with agitation reaches 70–90%, while without agitation it drops to 50–60%. This means that for the same treatment time, the agitated workpiece receives a significantly thicker and more uniform deposit.
Electroplating baths: specific requirements for each treatment type
Each stage of the electroplating cycle has different agitation needs. Let us examine the main ones.
Alkaline degreasing
Degreasing is the first stage of the cycle and uses strongly alkaline solutions (NaOH 30–50 g/l, carbonates, phosphates, surfactants) at temperatures of 50–80°C. Agitation must be vigorous to promote detachment of organic contaminants from the workpiece surface, keep surfactants in emulsion and ensure uniform cleaning across the entire surface.
For this stage, a high-speed EV series agitator with a three-blade marine propeller impeller in PP is the standard choice. The high speed generates the turbulence needed to “strip” oily residues from the metal surface.
Acid pickling
Pickling removes oxides and scale from the surface through immersion in strong acids: 10–20% hydrochloric acid (the most common), 10–25% sulfuric acid, or hydrochloric/hydrofluoric acid blends for stainless steels.
Agitation must be moderate: sufficient to maintain uniform acid concentration and remove reaction products (metal salts) from the surface, but not so violent as to cause excessive base metal removal. The EVR series with pitched blade impeller at low speed (50–150 rpm) is ideal: it generates recirculation without excessive turbulence.
For baths with hydrofluoric acid, the material must be PVDF. For dilute hydrochloric and sulfuric acid, PP is adequate.
Alkaline zinc bath
Alkaline zinc plating uses sodium zincate solutions in a strongly alkaline environment (NaOH 80–140 g/l) at ambient or slightly heated temperature (25–35°C). Agitation must be gentle and uniform to avoid localised turbulence that would cause non-uniform deposits.
A low-speed EVR or KVRL series agitator at 30–80 rpm with PP pitched blade impeller is ideal. PP has excellent resistance to caustic soda, even concentrated — one of the few applications where PP outperforms PVDF.
Nickel bath (Watts)
The Watts bath (nickel sulfate, nickel chloride, boric acid) operates at 45–55°C and pH 3.5–4.5. Agitation must be uniform and low-turbulence to prevent air incorporation and ensure a bright, pit-free deposit.
The EVR series at 40–100 rpm with PP impeller is the typical configuration. For electroless nickel baths that operate at 85–90°C with more aggressive pH, PVDF offers greater reliability.
Chrome plating bath
Chrome plating is the most critical electroplating process from both the agitation and materials standpoint. The bath contains chromic acid (CrO₃ 200–400 g/l) and sulfuric acid as catalyst, at temperatures of 50–60°C.
Chromic acid is a strong oxidiser that attacks both PP and PVC. PVDF is the only adequate thermoplastic material for agitators immersed in chrome plating baths.
Agitation must be moderate and uniform: sufficient to maintain homogeneous temperature and constant ion distribution, but without excessive turbulence that would promote evaporation of chromium compounds (an environmental and health concern). The EVR or KVRL series with PVDF impeller at 30–60 rpm is the optimal configuration.
Acid copper bath
Acid copper plating (copper sulfate in sulfuric acid) operates at ambient temperature with H₂SO₄ concentrations of 5–10%. Agitation must be vigorous near the cathodes to uniformise ion distribution, especially on workpieces with complex geometries (holes, recesses, corners).
The EV series with PP impeller at medium-high speed (300–800 rpm) provides the turbulent flow needed. For plants with large tanks, side-entry agitators from the LVO series may be preferable.
Rinsing and washing
Rinse tanks between process stages require vigorous agitation to rapidly remove chemical drag-out from the workpiece surface. High-speed EV series in PP, with the possibility of multiple installations for large tanks.
Installation configurations for electroplating tanks
Electroplating tanks have specific geometries (typically rectangular, long and narrow) that require particular installation solutions.
Top-entry installation
Top-entry installation is the most common for small and medium tanks. The agitator is mounted on the tank rim with a bracket support. The shaft descends vertically into the solution with the impeller positioned in the lower third of the tank.
For electroplating tanks, Nuova Darimpianti offers the EVL and EVRL series with extended shafts, specifically designed to reach the bottom of deep tanks without requiring intermediate guides.
Side-entry installation
For long tanks where a single top-entry agitator cannot guarantee uniformity along the entire length, side-entry installation (LVO or LRO series) generates a helical flow involving the entire volume. This configuration is particularly effective for electroplating lines with tanks 2–5 metres in length.
Multiple installation
For very large tanks or processes requiring particularly uniform agitation, multiple agitators can be installed on the same tank, distributed evenly along the length. In this case, it is important that the impellers generate complementary (not opposing) flows to avoid zones of excessive turbulence or dead zones.
Fume resistance: an often-overlooked aspect
In hot electroplating tanks, the zone immediately above the liquid level is exposed to concentrated acid fumes and vapours. The agitator shaft passes through this zone and suffers chemical attack that is different from — and often more aggressive than — the attack in the solution.
Chromic acid fumes, for example, attack PP even when the solution below would not (because the fumes are more concentrated and oxidising). For this reason, in chrome plating tanks it is advisable to use PVDF also for the exposed portion of the shaft, or to provide a protective sleeve in the liquid-vapour interface zone.
Agitator maintenance in electroplating environments
The electroplating environment is particularly aggressive for maintenance. Here are the recommended practices.
The impeller and shaft should be visually inspected every 3–6 months for signs of chemical attack (whitening, surface roughness, swelling). Bath concentration and temperature must be constantly monitored: a concentration drift can shift the fluid outside the material’s compatibility zone. Bearings and seals (in gear-reducer versions) must be protected from acid vapours with bellows or sleeves.
Thanks to solid-block CNC machining, Nuova Darimpianti components have no internal stresses that could accelerate chemical degradation: this translates to longer service life compared to moulded components, especially in cyclic environments (tanks heated and cooled daily).
Frequently asked questions
What agitation speed is needed for an electroplating tank?
It depends on the bath type. For chrome and nickel plating, low speeds (30–100 rpm) with pitched blade impellers are ideal to avoid excessive turbulence. For degreasing and rinsing, higher speeds (300–800 rpm) with propeller impellers promote mechanical cleaning. The guiding principle is: deposition baths → low speed; preparation baths → high speed.
Can I use compressed air instead of a mechanical agitator?
Air agitation is a traditional alternative, but has disadvantages: it introduces oxygen into the bath (problematic for many processes), creates acid mists above the tank, does not allow precise control of mixing intensity, and has lower energy efficiency. Mechanical agitators offer more precise control and better efficiency, and are preferred in modern plants.
Which material should I use for an agitator in a chrome plating tank?
PVDF is the only adequate thermoplastic material for chrome plating baths. Chromic acid is a strong oxidiser that attacks both PP and PVC. PVDF resists chromic acid at all concentrations and operating temperatures of chrome plating (50–60°C).
Can the agitator damage workpieces in the tank?
If the impeller is too close to the workpieces hung on the cathode frame, excessive flow can cause non-uniform deposits on exposed edges (the “dog bone” effect). The impeller should be positioned at least 15–20 cm from the workpieces, in the lower third of the tank, where it generates circulation without directly impinging on the cathode surfaces.
Does Nuova Darimpianti supply agitators for complete electroplating lines?
Yes. Nuova Darimpianti designs agitation solutions for the entire electroplating line: degreasing, pickling, deposition baths, rinses and post-deposition treatments. Each tank is individually analysed for size, fluid, temperature and process objective, with personalised selection of series, material and speed.
The right agitator for every stage of the electroplating cycle
The quality of an electroplating treatment depends on many factors, but agitation is one that is too often underestimated. A correctly sized agitator built from the right material improves deposit uniformity, reduces rejects, increases cathode efficiency and extends bath life.
Nuova Darimpianti manufactures high-speed agitators (EV, EVK, EVL, KVL series) and low-speed agitators (EVR, EVRK, EVRL, KVRL series) in PP, PVC and PVDF specifically designed for the electroplating and surface treatment industry. Every component is machined from solid blocks on CNC centres to guarantee maximum chemical resistance and durability even in the most aggressive baths.
Planning a new electroplating line or looking to improve agitation in existing tanks? Contact Nuova Darimpianti’s engineering team for personalised advice.
The choice between a fast and a slow agitator is not a matter of personal preference. It is dictated by the physics of the fluid inside the tank — above all, by its viscosity.
Install a fast agitator in a tank of viscous resin and you will see an impressive vortex around the shaft while the bulk of the liquid sits motionless against the walls. The impeller spins at full speed, the motor draws full power, and the process achieves nothing. Conversely, install a slow agitator in a low-viscosity acid bath and you will wait hours for a concentration that a fast unit would have homogenised in minutes. In both cases the cost is the same: wasted energy, extended batch times, inconsistent product quality, and — in corrosive chemical environments — accelerated wear on components that are far from inexpensive to replace.
Getting the speed category right is therefore the first and most consequential decision in any agitator selection project. This guide provides a practical framework for that decision, grounded in the relationship between fluid viscosity, flow regime and impeller geometry. It covers the full range of agitators manufactured by Nuova Darimpianti — from the high-speed EV series to the geared slow-speed KVRL series — and explains how to match each to the process it serves.
Viscosity and flow regime: the basis of selection
Before discussing impeller types or motor power, it is essential to understand the physical property that governs every mixing decision: viscosity.
What viscosity means for mixing
Dynamic viscosity (μ) is the measure of a fluid’s resistance to shear deformation — in plain terms, how strongly the fluid resists being stirred. It is expressed in millipascal-seconds (mPa·s), which is numerically equivalent to the older unit centipoise (cP). The higher the viscosity, the more energy an impeller must transfer to set the fluid in motion.
To put the numbers in perspective, consider these common industrial fluids:
Water: 1 cP — flows freely, negligible resistance to stirring
30 % sulphuric acid (H₂SO₄): ≈ 3 cP — slightly more viscous than water, still very fluid
Epoxy resins and polymer solutions: 10,000+ cP — semi-solid behaviour, extreme resistance to flow
The difference between 1 cP and 10,000 cP is not merely quantitative; it changes the fundamental character of the flow inside the tank.
The Reynolds number: predicting flow behaviour
The parameter that links viscosity to mixing performance is the impeller Reynolds number, defined as:
Re = ρ × N × D² / μ
Where ρ is the fluid density (kg/m³), N is the impeller rotational speed (rev/s), D is the impeller diameter (m) and μ is the dynamic viscosity (Pa·s). This dimensionless number indicates whether the flow in the tank is turbulent, transitional or laminar:
Re > 10,000 — Turbulent flow. The fluid moves chaotically in all directions, producing rapid and thorough mixing. Fast agitators thrive here.
10 < Re < 10,000 — Transitional flow. A mix of orderly and chaotic motion. The choice between fast and slow depends on the specific process requirements and impeller design.
Re < 10 — Laminar flow. The fluid moves in smooth, parallel layers with almost no cross-mixing. Only large, slow impellers can sweep the entire tank volume effectively.
Practical viscosity thresholds
While the Reynolds number is the theoretically correct criterion, plant engineers need quick rules. As a practical guideline for standard tank geometries and impeller sizes:
Below 500 cP → fast agitator (turbulent regime is readily achieved)
500–5,000 cP → transitional zone — evaluate case by case; sometimes a fast unit with inverter speed control or a moderate slow unit is appropriate
Above 5,000 cP → slow agitator (turbulence is impossible at reasonable power inputs; laminar mixing with large impellers is the only effective strategy)
These thresholds are approximate and depend on tank size, impeller diameter and rotational speed, but they provide a reliable starting point for the fast vs slow agitators decision.
Fast agitators: when and why
Fast agitators operate between 300 and 1,400 rpm, generating intense turbulence and high shear rates in the fluid. They are the default choice for low-viscosity applications where rapid blending, suspension and dispersion are required.
Operating principle
At high rotational speeds, a relatively small impeller generates strong velocity gradients in the fluid. These gradients break up concentration differences, suspend solid particles, shear droplets into smaller sizes and promote gas absorption. The resulting turbulence ensures that the entire tank volume is mixed, provided the viscosity is low enough for the turbulence to propagate outward from the impeller zone.
Applications best suited to fast agitators
Blending and dilution: mixing two or more miscible liquids of similar viscosity — for example, diluting concentrated sulphuric acid with water, or blending multiple chemical streams before a reactor
Solids suspension: keeping solid particles (salts, pigments, catalysts) in uniform suspension to prevent settling and ensure consistent downstream processing
Gas dispersion: drawing gas into the liquid and breaking it into fine bubbles — essential in aeration, neutralisation and certain reaction processes
Emulsification: creating stable emulsions of immiscible liquids by shearing one phase into fine droplets within the other
Heat transfer enhancement: turbulent flow at the tank wall dramatically increases the heat transfer coefficient, improving the performance of heating jackets and cooling coils
Impeller types for fast agitators
Nuova Darimpianti equips its fast agitator lines with three principal impeller geometries, each optimised for a different task:
Marine propeller (3-blade): the most common choice for general-purpose blending and dilution. It produces predominantly axial flow (top-to-bottom circulation), which is ideal for tank turnover and solids suspension. Used in the majority of rinsing, degreasing and acid dilution applications.
Cowles disc (high-shear disc): a flat disc with teeth or slots around the periphery, designed to produce extremely high shear at the impeller tip. Primarily used for dispersion of powders into liquids, pigment wetting and emulsification. Not suitable for viscous fluids, as the radial discharge quickly stalls at higher viscosities.
Turbine (radial flow): produces strong radial discharge and is effective for gas dispersion and intense local mixing. Often used when multiple impellers are mounted on a single shaft to cover the full tank height.
Nuova Darimpianti fast agitator series
The complete fast agitator range includes four models, each addressing a specific installation requirement:
EV series: the base fast agitator — top-mounted, direct-drive (EV-G version with coupling), suitable for the widest range of standard tank configurations
EVK series: fast agitator with aluminium lantern and bearing, self-aligning 7075 aluminium coupling and electric or pneumatic motor; fitted with a three-blade marine propeller
EVL series: fast agitator with aluminium lantern, single or double bearing and flexible or 7075 aluminium coupling (also as EVL-G); accepts marine propeller, straight-blade turbine, emulsifier or Cowles impellers
KVL series: heavy-duty fast agitator — cast iron lantern (single or double) with DCS angular-contact bearings, coupling or direct drive, electric motor only; accepts the same impellers as the EVL series
Typical industrial uses
In the chemical processing and surface treatment sectors that Nuova Darimpianti serves, fast agitators are routinely employed for degreasing baths, rinsing stations, acid and alkaline pickling, acid dilution, reagent dissolution and any application where the fluid viscosity remains below approximately 500 cP.
Slow agitators: when and why
Slow agitators operate between 10 and 150 rpm, producing laminar or mildly transitional flow with high pumping capacity and minimal shear. They are essential for any application involving viscous, shear-sensitive or delicate fluids.
Operating principle
At low rotational speeds, a large-diameter impeller sweeps through a broad cross-section of the tank, physically pushing the fluid in a controlled pattern. Instead of relying on turbulence to carry momentum outward, the impeller itself extends close to the tank wall and bottom, ensuring that even the most distant regions of the liquid are set in motion. The result is gentle but thorough bulk movement — exactly what viscous fluids require.
Applications best suited to slow agitators
Homogeneity maintenance: keeping already-mixed solutions uniform over long periods — critical in storage tanks, buffer vessels and recirculation loops
Shear-sensitive fluids: many polymers, biological solutions and crystal suspensions degrade or change properties when subjected to high shear. A slow agitator provides mixing without damage.
High-viscosity mixing: fluids above 5,000 cP cannot be mixed by a small, fast impeller — the turbulence simply does not propagate. A large anchor or helical ribbon impeller, rotating slowly, achieves top-to-bottom homogeneity.
Temperature uniformity: in heated or cooled tanks, slow agitators promote even temperature distribution without the localised hot or cold spots that can occur with fast units and viscous media
Crystallisation and precipitation: controlled, low-shear agitation allows crystals to grow uniformly without being broken by turbulence, improving yield and crystal size distribution
Impeller types for slow agitators
Pitched blade (wide blade, low angle): a large-diameter impeller with blades pitched at a shallow angle, producing predominantly axial flow at low speed. Effective for moderate viscosities (500–5,000 cP) and general-purpose slow mixing.
Anchor: a rectangular or U-shaped impeller that follows the contour of the tank wall, scraping or sweeping the boundary layer. Essential for preventing build-up on heated or cooled walls and for mixing fluids where wall effects dominate (high-viscosity creams, pastes, suspensions).
Helical ribbon: a continuous ribbon wound helically around the shaft, occupying nearly the full tank diameter and height. The most effective impeller geometry for extremely high viscosities (10,000+ cP), providing both axial and radial flow throughout the entire volume. Typically used for polymer solutions, adhesives, and thick slurries.
Nuova Darimpianti slow agitator series
EVR series: the base slow agitator — top-mounted with integrated gearbox, the workhorse of the slow range
EVRK series: slow agitator with gearbox and aluminium lantern for medium loads, with bearing; four-blade pitched, straight or high-flow impellers
EVRL series: slow agitator with gearbox and aluminium lantern for high loads, with bearing; same impeller options as the EVRK series
KVRL series: heavy-duty slow agitator — flanged shaft and cast iron lantern with bearing for heavy loads, 2 to 4 two- or four-blade impellers, optional ebonite lining; used in the most demanding viscous-fluid applications
Typical industrial uses
In the sectors served by Nuova Darimpianti, slow agitators are the standard for electroplating baths (chrome, nickel, zinc — where uniform concentration and temperature are critical to deposit quality), viscous chemical storage, polymer and resin processing, crystallisation tanks and any application where product integrity depends on gentle handling.
Direct comparison: the fast vs slow agitators decision table
The following table summarises the key differences between fast and slow agitators to support rapid selection:
When the fluid viscosity falls in the transitional zone (500–5,000 cP) and neither category seems clearly correct, the safest approach is: choose the slow agitator. The reasoning is straightforward. A slow agitator operating on a moderate-viscosity fluid will still achieve mixing — it may simply take a little longer. But a fast agitator operating on a fluid that is too viscous will create a dramatic vortex around the shaft while the bulk of the liquid remains stagnant. The visual impression is of vigorous mixing, but the process result is failure. You can always increase the speed of a slow unit with a variable-frequency drive; you cannot make a fast agitator with an undersized impeller sweep the full tank volume, no matter how fast it turns.
This principle is especially important in corrosive environments, where an agitator that churns without mixing wastes energy and subjects the thermoplastic components to unnecessary mechanical stress.
Tank geometry considerations
The performance of any agitator depends not only on the fluid but also on the geometry of the vessel in which it operates. Three geometric factors are particularly relevant to the fast vs slow agitators decision.
Impeller-to-tank diameter ratio (D/T)
The ratio of the impeller diameter (D) to the tank diameter (T) is a fundamental design parameter:
Fast agitators use impellers with D/T ratios between 0.2 and 0.4. The impeller is significantly smaller than the tank, relying on turbulence to distribute momentum to the tank periphery.
Slow agitators use impellers with D/T ratios between 0.5 and 0.8. The impeller physically occupies a large fraction of the tank cross-section, directly sweeping the fluid rather than depending on turbulent transport.
If the tank is very large relative to the impeller, a fast agitator may fail to circulate the outer regions — a strong argument for moving to a slow unit with a larger impeller.
Tank aspect ratio (H/D)
Tall, narrow tanks (H/D > 1.5) present a challenge for single-impeller systems. A single fast impeller near the bottom may leave the upper portion poorly mixed. Solutions include multiple impellers on a single shaft — the KVRL slow series, for example, carries 2 to 4 impellers.
For squat, wide tanks (H/D < 0.8), a side-entry agitator may be more effective than a top-mounted unit. Nuova Darimpianti’s lateral agitator range — the LVO (fast side-entry) and LRO (slow side-entry) models — is specifically designed for large-diameter, low-height storage tanks and process vessels where a top-entry installation is impractical.
Baffles
Baffles are vertical plates mounted on the inside of the tank wall, typically four equally spaced baffles each with a width of about 1/12 of the tank diameter. Their function is to prevent solid-body rotation (the entire liquid mass spinning as a unit) and to convert tangential flow into axial and radial components.
Fast agitators almost always require baffles. Without them, a high-speed impeller creates a deep vortex that reduces mixing efficiency and can entrain air.
Slow agitators generally do not require baffles. At low Reynolds numbers, solid-body rotation is minimal, and the large impeller already sweeps most of the tank volume. In viscous fluids, baffles can actually be counterproductive, creating dead zones behind them where stagnant pockets of unmixed material accumulate.
Materials and chemical resistance
Both fast and slow agitators from Nuova Darimpianti are manufactured from the same three engineering thermoplastics used throughout the company’s pump and agitator range:
PP (polypropylene): good chemical resistance to a wide range of acids, alkalis and solvents; cost-effective; suitable for temperatures up to approximately 80 °C
PVC (polyvinyl chloride): excellent resistance to many inorganic acids and alkalis; good rigidity; temperature limit approximately 60 °C
PVDF (polyvinylidene fluoride): premium material with outstanding resistance to concentrated acids, oxidising chemicals and high temperatures (up to approximately 120 °C); the material of choice for the most aggressive environments
Material considerations specific to fast vs slow agitators
The speed category affects the mechanical and chemical demands on the material differently:
Fast agitators subject the impeller and shaft to higher centrifugal forces and vibration. Material strength, stiffness and fatigue resistance become important design considerations. PVDF, with its superior mechanical properties, is often preferred for high-speed applications in aggressive media.
Slow agitators operate under lower mechanical stress but are typically immersed in the fluid continuously for long periods. Long-term chemical resistance and creep behaviour are the dominant material selection criteria. PP and PVC perform well in many slow-agitation applications; PVDF is specified when the chemical environment is particularly harsh.
CNC solid-block machining advantage
All Nuova Darimpianti agitator components — shafts, impellers, couplings, bearing housings — are machined from solid blocks of thermoplastic on CNC centres, not welded from sheet or moulded. This manufacturing method eliminates weld seams (which are stress concentration points and preferential corrosion sites), ensures dimensional accuracy, and produces components with homogeneous material properties throughout their cross-section. The advantage is significant for both fast and slow agitators, but it is especially critical for fast units where centrifugal forces amplify any structural weakness.
Frequently asked questions
What agitator speed do I need for a fluid with 100 cP viscosity?
A fluid at 100 cP is well within the fast agitator range. In a standard tank with a marine propeller impeller, the Reynolds number at 700–1,000 rpm will comfortably exceed 10,000, indicating fully turbulent flow. An EV series or EVK series agitator with a marine propeller is the typical choice. Only if the fluid is shear-sensitive (for instance, certain polymer solutions that are low-viscosity but degrade under shear) might a slow unit be appropriate at this viscosity.
Can I use a fast agitator for a chrome plating bath?
Chromium plating electrolytes are typically low-viscosity (close to water), which might suggest a fast agitator. However, chrome baths demand extremely uniform temperature and concentration profiles, and excessive turbulence at the surface can increase harmful chromic acid mist emissions. For this reason, electroplating baths almost always use slow agitators — an EVR series with a pitched blade impeller operating at 30–80 rpm — to provide gentle, uniform circulation without surface disturbance.
How do I calculate the Reynolds number for an agitator?
Use the formula Re = ρ × N × D² / μ, where ρ is the fluid density in kg/m³, N is the impeller rotational speed in revolutions per second (not per minute — divide rpm by 60), D is the impeller diameter in metres and μ is the dynamic viscosity in Pa·s (divide cP by 1,000). For example, for water (ρ = 1,000 kg/m³, μ = 0.001 Pa·s) with a 0.3 m impeller at 600 rpm (10 rev/s): Re = 1,000 × 10 × 0.09 / 0.001 = 900,000 — strongly turbulent. For glycerol (μ = 1.5 Pa·s) under the same conditions: Re = 1,000 × 10 × 0.09 / 1.5 = 600 — transitional, likely requiring a slow agitator.
What is the difference between a propeller and a pitched blade impeller?
Both produce axial flow (top-to-bottom circulation), but they are designed for entirely different speed regimes. A marine propeller is a small, three-bladed, high-speed impeller (D/T = 0.2–0.4) that generates flow through lift, much like an aircraft propeller. It is highly efficient in turbulent conditions but stalls in viscous fluids. A pitched blade impeller is a large-diameter, wide-blade impeller (D/T = 0.5–0.8) that pushes fluid by direct displacement at low speed. It works in transitional and laminar regimes where a propeller would be ineffective. In short: propellers are for fast agitators; pitched blades are for slow agitators.
Does Nuova Darimpianti offer variable speed agitators?
Yes. Any agitator in the Nuova Darimpianti range — fast or slow — can be supplied with a variable-frequency drive (VFD, also known as an inverter) that allows continuous adjustment of the motor speed. This is particularly useful in applications where viscosity changes during the process (for example, as temperature rises or as reagents are added), or where the same tank handles different products at different times. The KVL series (fast) and KVRL series (slow) are heavy-duty agitators well suited to variable-speed operation; on the KVRL, as on all slow agitators, the gearbox provides additional torque at reduced speeds.
Choosing the right agitator starts with understanding the fluid
The fast vs slow agitators decision is, at its core, a question about fluid viscosity and the flow regime it produces. Low-viscosity fluids in turbulent conditions respond to small, fast impellers. High-viscosity fluids in laminar conditions require large, slow impellers. The transitional zone demands careful evaluation — and when in doubt, choosing slow is the safer path.
Nuova Darimpianti manufactures both categories in the same corrosion-resistant thermoplastic materials (PP, PVC and PVDF), using the same CNC solid-block machining process, ensuring that chemical resistance and mechanical integrity are never compromised regardless of the speed category selected.
If you are unsure whether your application calls for a fast or slow agitator — or if your fluid sits in the transitional zone — contact the Nuova Darimpianti engineering team. With detailed knowledge of every series in the range, they can evaluate your fluid properties, tank geometry and process requirements and recommend the agitator configuration that delivers reliable, energy-efficient mixing in even the most aggressive chemical environments.
How to Choose an Industrial Agitator: A Practical Sizing Guide
Choosing an industrial agitator is not simply a matter of buying a motor with a propeller. An undersized agitator will leave dead zones in the tank where the product remains unmixed, causing process defects.
An oversized agitator will waste energy, generate excessive vibrations and shorten the service life of bearings and shaft.
Correct sizing requires a systematic analysis that starts from the fluid properties and process conditions and works towards the choice of impeller, rotational speed and motor power.
This technical guide covers every step of the selection process, with reference to the agitator series manufactured by Nuova Darimpianti for corrosive environments.
Starting point: what the agitator needs to achieve
Before discussing impellers and motors, it is essential to clearly define the purpose of the agitation process. Different operations require very different approaches.
Homogeneous blending is the most common operation: uniformising the composition of a liquid within the tank, typically after a reagent addition. It requires good circulation of the entire volume with moderate turbulence.
Solid suspension requires the agitator to generate sufficient fluid velocity to prevent solid particles from settling on the tank bottom. The power needed depends on particle density and size distribution.
Gas-liquid dispersion applies to processes such as aeration in biological treatment or chemical reactions with gaseous reagents. It requires high-turbulence impellers capable of breaking gas bubbles into microbubbles to maximise the exchange surface area.
Heat transfer requires the agitator to maintain a constant flow along the tank walls where cooling or heating coils or jackets are installed.
Emulsification (creating stable liquid-liquid emulsions) requires high shear forces to reduce the droplet size of the dispersed phase.
Clearly defining the objective is the first step: the required flow pattern, the most suitable impeller and the power demand all follow from it.
The fluid properties that drive the selection
The two physical properties that most influence agitator sizing are viscosity and density.
Viscosity: the dominant parameter
Viscosity measures a fluid’s internal resistance to flow. A low-viscosity fluid such as water (1 cP) behaves radically differently from a heavy oil (10,000 cP) or a resin (100,000 cP).
For low-viscosity fluids (1–100 cP), such as aqueous solutions, dilute acids and solvents, the flow regime is easily turbulent and agitation is relatively straightforward. Small-diameter, high-speed impellers are sufficient (D/T ratio between 0.2 and 0.4, where D is the impeller diameter and T the tank diameter).
For medium-viscosity fluids (100–10,000 cP), such as concentrated suspensions, emulsions and polymer solutions, the transitional regime makes mixing more complex. Larger-diameter impellers (D/T between 0.4 and 0.6) at intermediate speeds are required.
For high-viscosity fluids (above 10,000 cP), such as pastes, gels, adhesives and resins, the regime is laminar and conventional impellers become ineffective. Large-diameter impellers that approach the tank walls (D/T between 0.6 and 0.95), such as anchors or helical ribbons, operating at very low speeds are needed.
Density: the effect on power
The fluid density (expressed in kg/m³) directly affects the power drawn by the agitator. All other parameters being equal, doubling the density doubles the required power. For concentrated acids (density 1,400–1,840 kg/m³ for sulfuric acid) the power demand is significantly higher than for aqueous solutions.
Rheological behaviour
Many industrial fluids do not have a constant viscosity — they are non-Newtonian fluids. Some become less viscous when agitated (pseudoplastic or shear-thinning fluids), others become more viscous (dilatant or shear-thickening fluids), and others have a yield stress that must be exceeded before the fluid moves (Bingham plastic fluids). Understanding the rheological behaviour is essential for correct agitator sizing.
The rotational Reynolds number: the sizing compass
The parameter that links fluid properties to agitator operating conditions is the rotational Reynolds number, defined as:
Re = (ρ × N × D²) / μ
where ρ is the fluid density (kg/m³), N the impeller rotational speed (revolutions per second), D the impeller diameter (m) and μ the dynamic viscosity (Pa·s).
The Reynolds number determines the flow regime inside the tank. At Re < 10, the regime is laminar: the fluid moves in ordered layers and mixing occurs mainly by molecular diffusion. At 10 < Re < 10,000, the regime is transitional: laminar and turbulent zones coexist, and mixing is uneven. At Re > 10,000, the regime is fully turbulent: mixing is rapid and efficient, with optimal mass and heat transfer.
The sizing objective is to select the impeller-speed combination that brings the Reynolds number into the desired regime for the specific process. For homogeneous blending in turbulent conditions, Re > 10,000 is the minimum target.
Impeller types: axial, radial and tangential flow
The impeller is the heart of the agitator. Its geometry determines the type of flow generated in the tank and, consequently, the effectiveness of the mixing process.
Axial flow impellers
Axial flow impellers drive the fluid parallel to the agitator shaft, generating a large recirculation loop that involves the entire tank volume. They are the most efficient for homogeneous blending and solid suspension, because they move large fluid volumes with relatively low energy consumption.
The main types include the three-blade marine propeller, the classic choice for low to medium-viscosity fluids. Nuova Darimpianti’s EV series features three-blade marine propeller impellers in PP, PVC or PVDF for corrosive environment applications, with rotational speeds up to 1,400 rpm. It is the quintessential high-speed agitator, ideal for blending, neutralisation and dilution tanks for acids and bases.
Pitched blade impellers combine a dominant axial component with a radial component, offering versatility in applications requiring both circulation and a degree of localised turbulence.
Radial flow impellers
Radial flow impellers drive the fluid perpendicular to the agitator shaft, towards the tank walls. They generate high shear forces in the zone immediately surrounding the impeller, making them ideal for gas-liquid dispersion, emulsification and solid dissolution.
The Cowles impeller (or sawtooth disc) is a disc with a serrated perimeter that generates an intense shear zone. It is the preferred choice for pigment dispersion in paints, emulsion preparation and mixing of fluids with very different viscosities. Nuova Darimpianti’s EVK series features a three-blade marine propeller; for applications requiring high shear in corrosive environments, the Cowles impeller is available on the EVL and KVL series and on the LVO side-entry agitators.
Flat blade turbines (Rushton type) generate intense radial flow and are the standard for gas-liquid dispersion in chemical reactors and bioreactors.
High-viscosity impellers
For high-viscosity fluids, conventional impellers (axial and radial) cannot generate adequate flow because turbulence does not propagate far from the impeller. In these cases, large-diameter impellers such as anchors and helical ribbons are used, operating at very low speeds (5–50 rpm) but involving the entire tank volume due to their proximity to the walls.
Axial and radial flow patterns in industrial mixing
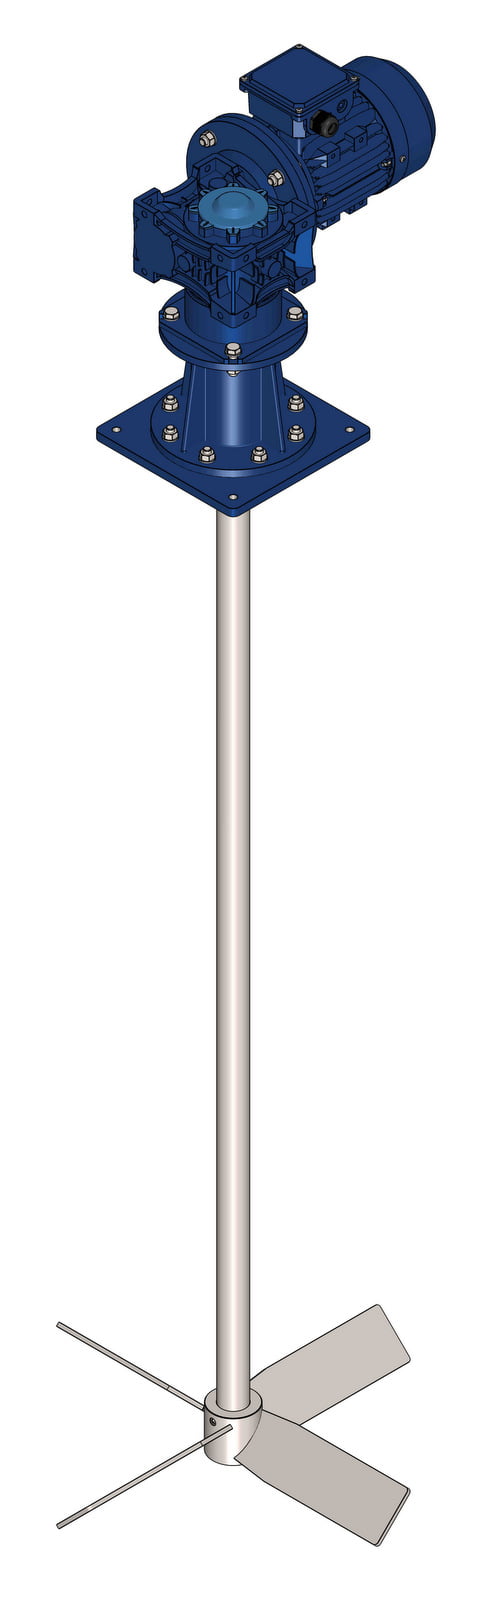
Three-blade marine propeller impeller in PVDF for EV high-speed agitator
High-speed and low-speed agitators: the Nuova Darimpianti range
Nuova Darimpianti classifies its agitators into two main families based on rotational speed, each designed for a specific application range.
High-speed series: EV, EVK, EVL, KVL
High-speed series agitators operate at high rotational speeds (typically 300 to 1,400 rpm) and feature impellers with a relatively small diameter compared to the tank.
The EV series is the standard high-speed agitator with a three-blade marine propeller impeller, ideal for homogeneous blending, dilution and neutralisation of low to medium-viscosity fluids. The EVK series has an aluminium lantern with bearing and a self-aligning 7075 aluminium coupling, an electric or pneumatic motor and a three-blade marine propeller. The EVL series has an aluminium lantern with single or double bearing and a flexible or 7075 aluminium coupling, and accepts marine propeller, straight-blade turbine, emulsifier or Cowles impellers. The KVL series is the heavy-duty version, with a cast iron lantern (single or double), DCS angular-contact bearings, coupling or direct drive and electric motor only; it accepts the same impellers as the EVL series.
All high-speed models are available with shaft and impeller in PP, PVC, PVDF or AISI 316 stainless steel, and are fitted with a three-phase electric motor; some series, such as the EVK, are also available with a pneumatic motor, while the KVL is electric only.
Low-speed series: EVR, EVRK, EVRL, KVRL
Low-speed series agitators operate at reduced rotational speeds (5 to 380 rpm via a mechanical gear reducer) and feature larger-diameter impellers, generating a gentler but more penetrating flow throughout the tank volume.
The EVR series is the standard low-speed agitator with a four-blade pitched impeller, designed for gentle blending, suspension maintenance and slow recirculation of shear-sensitive fluids. The EVRK series combines the gearbox with an aluminium lantern for medium loads and a bearing, and accepts four-blade pitched, straight or high-flow impellers. The EVRL series is the version with gearbox and aluminium lantern for high loads, with bearing and the same impellers as the EVRK. The KVRL series is the heavy-duty version, with flanged shaft and cast iron lantern with bearing; it carries 2 to 4 two- or four-blade impellers and is available with ebonite lining.
The low-speed series application range spans viscous solutions to suspensions with heavy solids, from electroplating to water treatment.
Side-entry series: LVO and LRO
For large-volume tanks where top-entry installation is not practical, Nuova Darimpianti offers side-entry agitators mounted on the tank wall. The LVO series is the high-speed version; the LRO series is the low-speed version with gear reducer. Both generate a helical flow pattern inside the tank that ensures effective mixing even in large-diameter cylindrical vessels.
Practical sizing: the parameters to define
Once the impeller type has been chosen, agitator sizing requires the determination of four fundamental parameters.
1. Impeller diameter
The D/T ratio (impeller diameter / tank diameter) is the first parameter to establish. For high-speed agitators with axial flow impellers, the typical ratio is 0.25–0.40. For low-speed agitators with pitched blade impellers, the ratio rises to 0.40–0.65. For anchor or ribbon impellers, it reaches 0.90–0.98.
2. Rotational speed
Speed is chosen based on the desired Reynolds regime and impeller type. High-speed impellers (propellers, turbines) operate between 300 and 1,400 rpm. Low-speed impellers (pitched blades) between 20 and 380 rpm. High-viscosity impellers between 5 and 50 rpm.
3. Motor power
The required power is calculated through the power number (Np), a dimensionless coefficient characteristic of each impeller type:
P = Np × ρ × N³ × D⁵
where P is power (W), Np the impeller power number, ρ the fluid density (kg/m³), N the rotational speed (rev/s) and D the impeller diameter (m).
The power number varies by impeller type: for a three-blade marine propeller it is approximately 0.3–0.5 in the turbulent regime, for a Rushton turbine approximately 4–6, and for a pitched blade impeller approximately 1.2–1.5.
A common mistake is selecting the motor based solely on rated kW. The critical parameter is the shaft torque (expressed in Nm), which determines the agitator’s ability to overcome fluid resistance. For viscous fluids, a powerful motor running at high speed may have less usable torque than a less powerful but slower motor fitted with a gear reducer.
4. Installation position and shaft length
The agitator must be correctly positioned within the tank. For axial flow impellers, the distance from the tank bottom should be approximately one impeller diameter. For tall tanks with a variable level, it may be necessary to install multiple impellers on the same shaft (the KVRL series, for example, carries 2 to 4).
Eccentric installation (with the agitator axis offset from the tank centre) or angled mounting is an effective alternative to baffles for preventing the central vortex in open tanks.
Material selection for corrosive environments
In environments where the fluid is chemically aggressive, the shaft and impeller material must be compatible with the process. Nuova Darimpianti manufactures agitators with shafts and impellers machined from solid blocks on CNC centres in the following thermoplastic materials.
Polypropylene (PP) is the standard choice for dilute acids, bases, saline solutions and electroplating baths up to 80°C. PVC is suitable for sodium hypochlorite and low-temperature solutions. PVDF offers superior chemical resistance for concentrated acids, solvents and oxidising environments up to 100°C. PE-HD (high-density polyethylene) is used for specific low-temperature applications.
Solid-block CNC machining ensures no internal stresses and precise dimensional tolerances — a critical advantage for impellers operating at high rotational speeds where even small imbalances generate excessive vibrations.
Common mistakes in agitator selection
Industry experience reveals several recurring errors in industrial agitator selection.
Selecting the agitator based on motor power rather than analysing the process. A 5 kW agitator with the wrong impeller can mix worse than a 1.5 kW unit with the correct one.
Ignoring viscosity changes during the process. Many processes involve viscosity variations during the cycle (for example during polymerisation or heating). The agitator must be sized for the most demanding condition.
Not accounting for variable tank level. If the tank is filled and emptied while the agitator is running, the impeller may be exposed above the liquid during low-level phases, causing vibrations, unwanted aeration and accelerated wear.
Underestimating the effect of baffles. In cylindrical tanks with axial impellers, the absence of baffles causes a central vortex that drastically reduces mixing effectiveness and can entrain air into the fluid.
What is the difference between a high-speed and a low-speed agitator?
A high-speed agitator typically operates between 300 and 1,400 rpm with a small impeller relative to the tank (D/T 0.2–0.4) and generates intense turbulent flow. A low-speed agitator operates between 5 and 380 rpm with a larger impeller (D/T 0.4–0.65) and generates a gentler but more extensive flow. The choice depends on fluid viscosity and the process type: high-speed for rapid mixing of low-viscosity fluids, low-speed for viscous or shear-sensitive fluids.
How do you calculate the power required for an agitator?
Power is calculated using the formula P = Np × ρ × N³ × D⁵, where Np is the impeller power number (a coefficient that depends on geometry), ρ the fluid density, N the speed and D the impeller diameter. The Np value is obtained from experimental correlations specific to each impeller type and Reynolds regime.
What happens if the fluid viscosity changes during the process?
The agitator must be sized for the most demanding condition. If viscosity increases during the process (for example in a polymerisation reaction), the agitator must be capable of generating sufficient torque even at maximum viscosities. A variable frequency drive (VFD) can be useful for adapting speed to different process stages.
Which materials are suitable for agitating acids in electroplating tanks?
For electroplating tanks with dilute acids and metal salt solutions, polypropylene (PP) is the standard choice. For baths containing chromic acid, hydrofluoric acid or strongly oxidising solutions, PVDF is required. Nuova Darimpianti manufactures shafts and impellers in PP, PVC, PVDF, PE-HD and Ebonite, all machined from solid blocks on CNC centres.
Can Nuova Darimpianti size the agitator for my specific application?
Yes. Correct sizing requires information about tank volume, fluid type and properties, process objective and operating conditions. Nuova Darimpianti’s engineering team analyses these data and proposes the optimal combination of series, impeller, material and motor for each application.
Choose the right agitator
Selecting an industrial agitator is a technical process requiring analysis of multiple factors: the process objective, fluid properties, the desired flow regime, tank geometry and operating conditions.
Nuova Darimpianti designs and manufactures high-speed agitators (EV, EVK, EVL, KVL series), low-speed agitators (EVR, EVRK, EVRL, KVRL series) and side-entry agitators (LVO, LRO series) in PP, PVC, PVDF and AISI 316 stainless steel, all with components machined from solid blocks on CNC centres. Every agitator can be custom-configured for the specific requirements of your plant.